
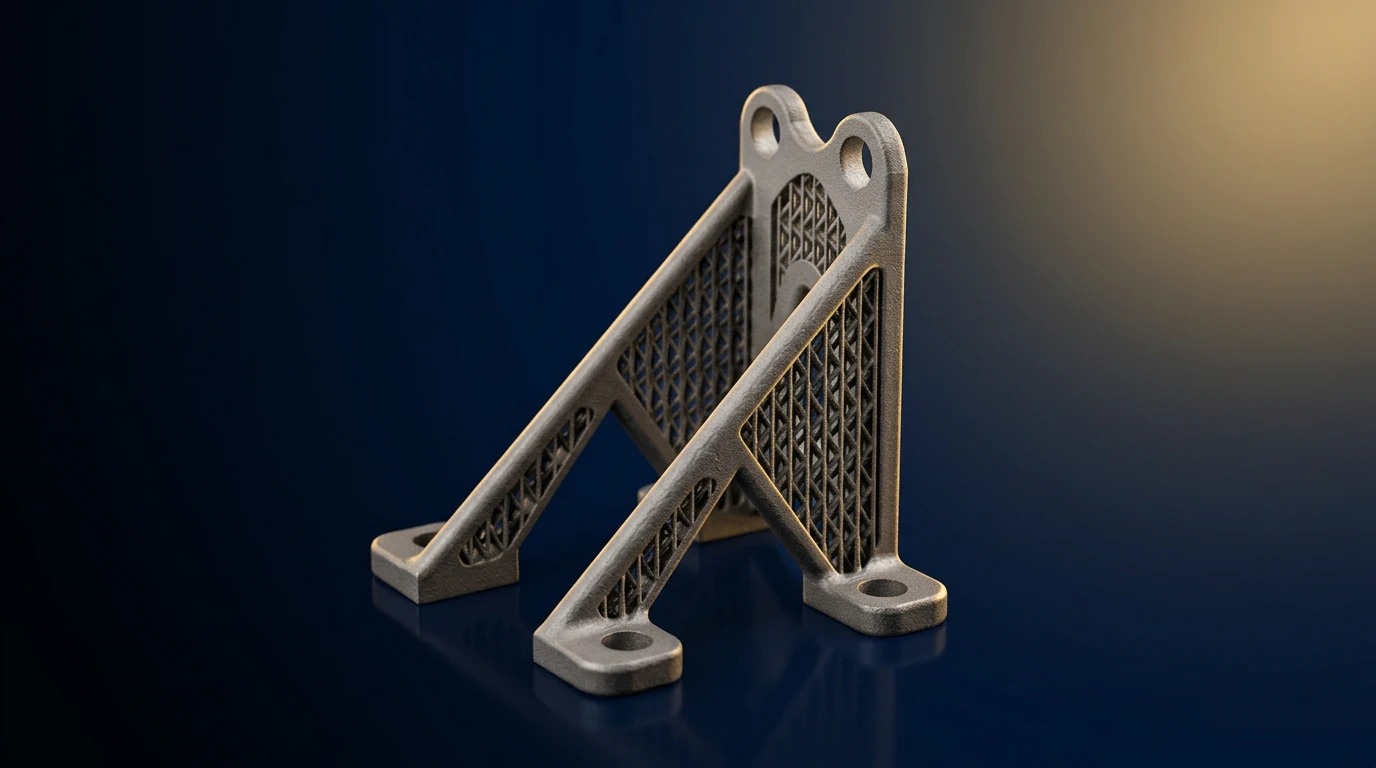
Laser powder bed fusion (LPBF) is the process behind almost every dense metal 3D-printed part in service today — the titanium brackets on aircraft, the Inconel hardware in engines, the patient-specific implants in spines. It builds a solid metal part directly from fine powder, one melted layer at a time. This guide explains how LPBF works, why it goes by several names, what it prints well, and where its limits are.
How laser powder bed fusion works
The process repeats one cycle for every layer of the part:
- Spread. A recoater blade sweeps a thin, even layer of metal powder — typically 20–60 microns thick — across the build plate.
- Melt. A high-power laser scans the cross-section of the part, melting the powder into fully dense metal and fusing it to the layer below.
- Lower. The build plate drops by one layer thickness, and the cycle repeats.
It all happens inside a sealed chamber filled with inert gas (argon or nitrogen), because molten metal would otherwise react with oxygen. After thousands of layers, the finished part is dug out of the surrounding loose powder, cut off the plate, and sent to post-processing.
LPBF, DMLS, SLM: same process, different names
The one nuance: “sintering” in DMLS is a misnomer — the metal is fully melted, not just sintered. LPBF is the neutral, standards-friendly term for the process family. If you see all three in a spec, they are asking for the same thing.
Typical LPBF process parameters
These are the levers an operator tunes on LPBF printers, working from gas-atomised metal powder. The values are typical ranges, not fixed settings — each alloy has its own tuned parameter set.
| Parameter | Typical range | Why it matters |
|---|---|---|
| Layer thickness | 20–60 µm | Trades resolution against build speed |
| Laser power | 200–1000 W | Sets melt-pool stability and throughput |
| Laser spot size | 70–100 µm | Limits the finest printable feature |
| Powder size (PSD) | 15–45 µm | Drives flowability and final density |
| Atmosphere | Argon or nitrogen (inert) | Prevents oxidation of the melt |
| Build rate | ~5–40 cm³/h | Depends on alloy and layer thickness |
What LPBF prints
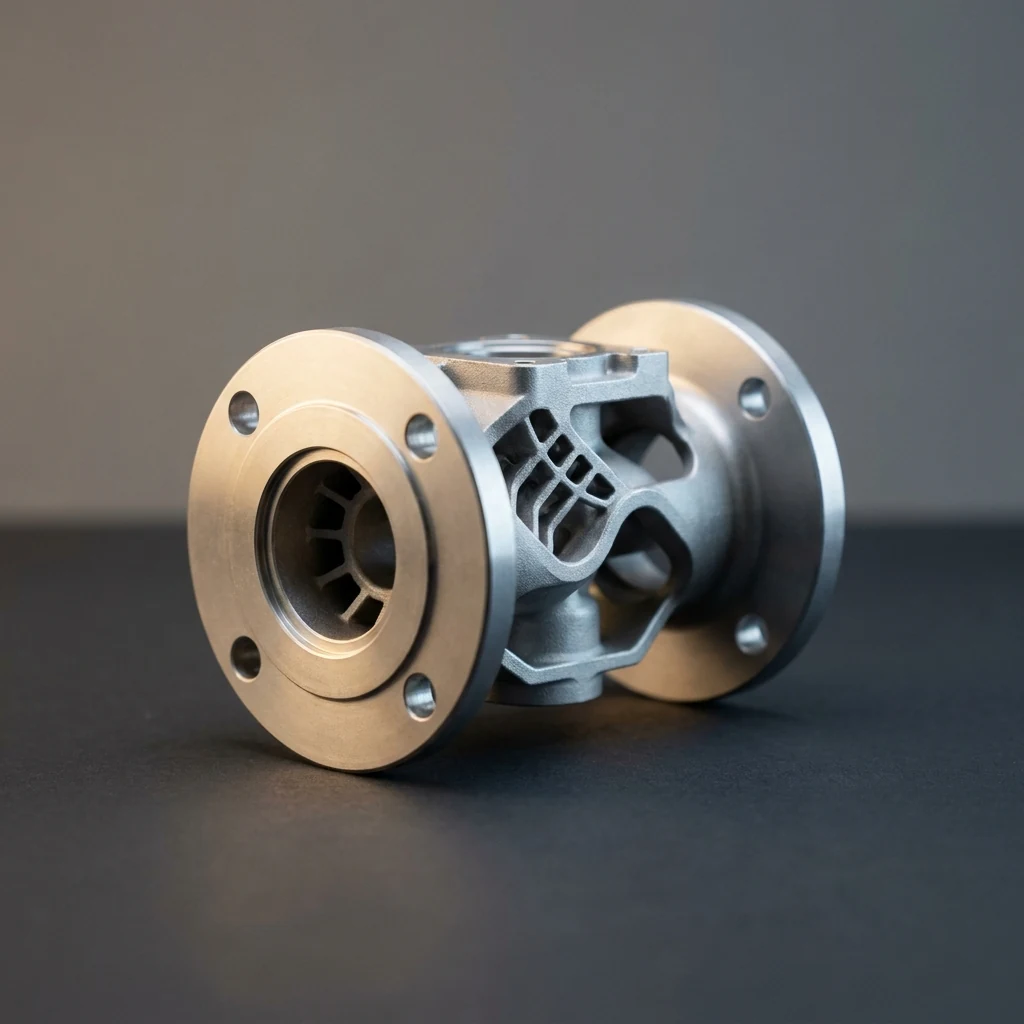
LPBF runs the workhorse metals of engineering: titanium Ti-6Al-4V for strength-to-weight, Inconel for high-temperature strength, aluminium AlSi10Mg for light housings, and stainless and tool steels for general work. What it does that machining and casting cannot is build fully dense parts with internal channels, lattices and consolidated geometry — the reason it dominates aerospace, medical and tooling. Browse the alloys as metal powders and the machines as LPBF printers.
What LPBF is good and bad at
Good at: dense, strong, complex metal parts in low volume; internal cooling channels; part consolidation; a wide alloy range. Limited by: build size (parts fit within the chamber), support structures on overhangs, the residual stress that heat builds into the part, and a mandatory post-processing chain. An LPBF part is never finished at the printer — stress relief, HIP, heat treatment and machining follow, and they need to be planned in from the design stage.
The full LPBF workflow
A part goes from model to metal in three stages: design for additive (orientation, supports, walls), the LPBF build itself, and post-processing to reach final properties and tolerance. Getting the first stage right makes the other two cheaper — and it is where most of the cost is decided.
If you are scoping a metal part, our engineers run it through this chain as a metal 3D printing service. New to additive? Start with what additive manufacturing is.
Frequently asked questions
What is laser powder bed fusion (LPBF)?
A metal 3D printing process that builds a fully dense part from fine metal powder, melting each thin layer with a laser inside an inert-gas chamber and fusing it to the layer below.
What is the difference between LPBF, DMLS and SLM?
They are the same laser-powder-bed process under different names, mostly vendor branding. The metal is fully melted in all of them; LPBF is the neutral term.
What metals can be printed with LPBF?
Titanium Ti-6Al-4V, nickel superalloys such as Inconel, aluminium AlSi10Mg, and stainless and tool steels, among others.
Does an LPBF part need post-processing?
Yes. Stress relief, hot isostatic pressing, heat treatment and finish machining are standard, and they should be planned in from the design stage.
Have a question or a project? Let’s talk.
Tell us what you need — a real applications engineer replies within 24 hours. NDA standard, no sales script.