
In stock
- Debind & sinter parameters + datasheet in every order
- Mutual NDA before any file or spec review
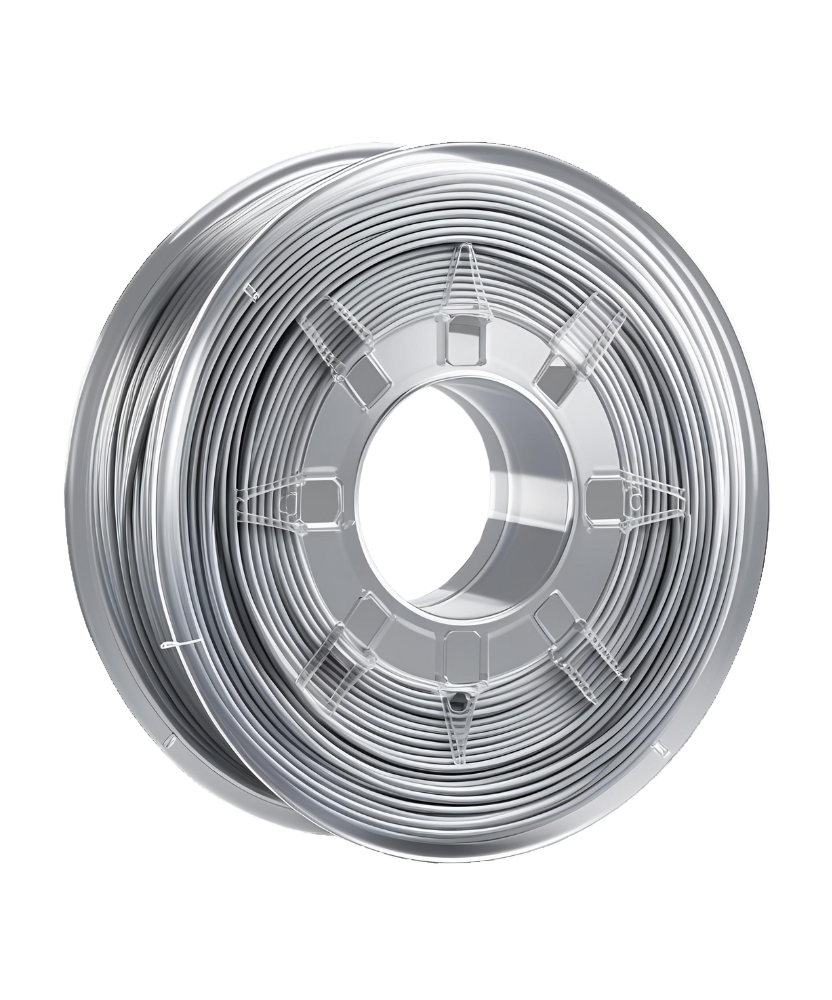
Fila-MAT Metal Titanium 1,75mm
Print titanium parts on 3DCeram's M.A.T. FFF platform, then debind and sinter to dense, high-strength, lightweight metal.
- ✔ Rp0.2 844 MPa, Rm 940 MPa at 4.33 g/cc after sintering — tested to ASTM E8/E8M
- ✔ Debind and sinter parameters plus the full datasheet included with every spool
- ✔ 1.75mm bound-metal feedstock for the 3DCeram M.A.T. FFF head — mutual NDA before any spec review
What your process engineer actually checks
Third-party mechanical data
Rp0.2 844 MPa, Rm 940 MPa at 4.33 g/cc density and a 118 GPa modulus after sintering, tested to ASTM E8/E8M. You qualify Fila-MAT Metal Titanium against measured numbers, not a filament-vendor estimate.
Debind and sinter parameters included
Every spool ships with 3DCeram's datasheet and the full print, debind and sinter cycle for the M.A.T. FFF head, so green parts reach target density on the first build instead of after trial-and-error.
A materials engineer on the line
Shrinkage, warpage and heat-treatment questions go to an engineer who has run bound-metal FFF — not a ticket queue. Sub-4h reply, mutual NDA standard before any spec review.
.tabs-section .tab-pane table{border-collapse:separate;border-spacing:0;width:100%;border:1px solid #E6E8EC;border-radius:12px;overflow:hidden;margin:18px 0;font-size:15px;line-height:1.45}.tabs-section .tab-pane table th,.tabs-section .tab-pane table td{border-bottom:1px solid #EFF1F4;border-right:1px solid #EFF1F4;padding:11px 14px;text-align:left;vertical-align:top;color:#23262B}.tabs-section .tab-pane table thead th{background:#F4F1E9;color:#1C2A3A;border-bottom:2px solid #D6B16F;font-weight:700;letter-spacing:.02em}.tabs-section .tab-pane table tbody th,.tabs-section .tab-pane table tbody td:first-child{background:#F7F8FA;font-weight:600;color:#101114}.tabs-section .tab-pane table tr td:last-child,.tabs-section .tab-pane table tr th:last-child{border-right:0}.tabs-section .tab-pane table tbody tr:last-child td{border-bottom:0}.tabs-section .tab-pane h2{border-left:3px solid #D6B16F;padding-left:12px;margin-top:30px}.tabs-section .tab-pane ul{list-style:square;padding-left:20px}.tabs-section .tab-pane ul li::marker{color:#D6B16F}.final-cta{display:none}.rev-section{display:none!important}.tabs-section .tab-pane figure{margin:24px auto;text-align:center;max-width:600px}.tabs-section .tab-pane figure img{max-width:600px;width:100%;height:auto;border-radius:14px;border:1px solid #F0EDE8}.tabs-section .tab-pane figcaption{font-size:12.5px;color:#8C877D;margin-top:7px}
.tab-pane .lead{font-size:15.5px;color:#5B5751;line-height:1.6;max-width:820px}
.tab-pane .desc-block{margin-top:32px}
.tab-pane .desc-block-head{margin-bottom:14px;max-width:780px}
.tab-pane .desc-block-head h4{font-size:17px;font-weight:800;letter-spacing:-.01em;color:#323131;margin:0 0 4px;position:relative;padding-left:14px}
.tab-pane .desc-block-head h4::before{content:””;position:absolute;left:0;top:5px;bottom:5px;width:3px;border-radius:2px;background:#D6B16F}
.tab-pane .desc-block-head .sub{font-size:13px;color:#8C877D;line-height:1.55;margin:0;padding-left:14px}
.tab-pane .tbl-note{font-size:12px;color:#8C877D;margin-top:-8px}
.tab-pane .feat-grid{display:grid;grid-template-columns:repeat(2,1fr);gap:14px 28px;margin-top:8px;padding-left:14px}
.tab-pane .feat-grid br,.tab-pane .app-chips br,.tab-pane .alt-grid br,.tab-pane .how-grid br{display:none}
.tab-pane .feat-tile{display:flex;gap:11px;align-items:flex-start}
.tab-pane .feat-tile .ft-ico{width:26px;height:26px;border-radius:6px;background:#FBF9F4;color:#5B5751;display:flex;align-items:center;justify-content:center;flex-shrink:0;margin-top:1px;border:1px solid #F0EDE8}
.tab-pane .feat-tile .ft-ico svg{width:14px;height:14px;fill:currentColor}
.tab-pane .feat-tile h5{font-size:13.5px;font-weight:700;color:#323131;margin:0 0 2px;line-height:1.3}
.tab-pane .feat-tile p{font-size:12.5px;color:#5B5751;line-height:1.5;margin:0}
.tab-pane .how-grid{display:grid;grid-template-columns:repeat(3,1fr);gap:24px;margin-top:8px;padding:22px 24px;background:linear-gradient(135deg,#070F22 0%,#0B1B3A 50%,#2D2A22 100%);border-radius:12px;position:relative;overflow:hidden;color:#fff}
.tab-pane .how-grid::before{content:””;position:absolute;top:0;left:0;right:0;height:3px;background:linear-gradient(90deg,#D6B16F 0%,#FFE2A6 50%,#D6B16F 100%)}
.tab-pane .how-step{position:relative;z-index:1}
.tab-pane .how-step .hs-n{font-family:”SF Mono”,ui-monospace,monospace;font-size:10px;font-weight:700;color:#D6B16F;letter-spacing:.1em;margin-bottom:6px;display:inline-flex;align-items:center;gap:6px;text-transform:uppercase}
.tab-pane .how-step .hs-n::before{content:””;width:14px;height:1px;background:#D6B16F}
.tab-pane .how-step h6{font-size:13.5px;font-weight:800;color:#fff;margin:0 0 4px;line-height:1.25}
.tab-pane .how-step p{font-size:12.5px;color:rgba(255,255,255,.78);line-height:1.5;margin:0}
.tab-pane .app-chips{display:grid;grid-template-columns:repeat(2,1fr);gap:9px 28px;margin-top:8px;padding-left:14px}
.tab-pane .app-chip{display:flex;align-items:center;gap:10px}
.tab-pane .app-chip .ac-ico{width:22px;height:22px;border-radius:5px;background:#FBF9F4;color:#5B5751;display:flex;align-items:center;justify-content:center;flex-shrink:0;border:1px solid #F0EDE8}
.tab-pane .app-chip .ac-ico svg{width:12px;height:12px;fill:currentColor}
.tab-pane .app-chip .ac-t{font-size:13px;color:#323131;font-weight:700}
.tab-pane .app-chip .ac-s{font-size:11.5px;color:#8C877D;font-weight:500;margin-top:1px}
.tab-pane .alt-grid{display:grid;grid-template-columns:repeat(3,1fr);gap:12px;margin-top:8px}
.tab-pane .alt-card{background:#fff;border:1px solid #EAE7E1;border-radius:10px;padding:14px 16px 13px;display:flex;flex-direction:column;gap:5px;position:relative;overflow:hidden;text-decoration:none;transition:border-color .2s,transform .2s,box-shadow .2s}
.tab-pane .alt-card::before{content:””;position:absolute;top:0;left:0;right:0;height:2px;background:#D6B16F;transform:scaleX(.15);transform-origin:left;transition:transform .3s}
.tab-pane .alt-card:hover{border-color:#D6B16F;transform:translateY(-2px);box-shadow:0 6px 16px rgba(20,16,8,.08)}
.tab-pane .alt-card:hover::before{transform:scaleX(1)}
.tab-pane .alt-card .ac-lbl{font-size:10.5px;font-weight:700;color:#8C877D;letter-spacing:.06em;text-transform:uppercase}
.tab-pane .alt-card .ac-name{font-size:15px;font-weight:800;color:#323131;line-height:1.2}
.tab-pane .alt-card .ac-meta{font-size:11.5px;color:#5B5751;line-height:1.4;margin-top:1px}
.tab-pane .alt-card .ac-cta{margin-top:8px;font-size:12px;color:#5B5751;display:inline-flex;align-items:center;gap:5px;font-weight:600;padding-top:8px;border-top:1px solid #F0EDE8}
.tab-pane .alt-card:hover .ac-cta{color:#323131}
.tab-pane .desc-close{margin-top:16px;padding:15px 20px;background:#FBF9F4;border-left:3px solid #D6B16F;border-radius:0 8px 8px 0;font-size:13.5px;color:#5B5751;line-height:1.55;max-width:820px}
.tab-pane .desc-close b{color:#323131;font-weight:700}
.tab-pane .desc-close .btn-spec{display:inline-flex;align-items:center;gap:7px;margin-top:12px;padding:10px 20px;border:0;border-radius:999px;background:linear-gradient(135deg,#FFBF00,#FF9000);color:#1C1A16;font-weight:700;font-size:13px;cursor:pointer;transition:transform .15s,box-shadow .15s}
.tab-pane .desc-close .btn-spec:hover{transform:translateY(-1px);box-shadow:0 6px 14px rgba(255,144,0,.35)}
@media(max-width:760px){.tab-pane .feat-grid,.tab-pane .app-chips,.tab-pane .alt-grid,.tab-pane .how-grid{grid-template-columns:1fr}}
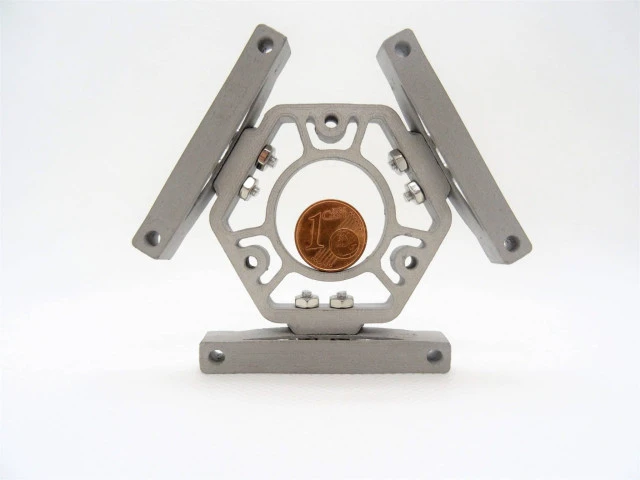
Fila-MAT Metal Titanium is 3DCeram’s bound-metal FFF feedstock — 1.75mm filament loaded with Ti6Al4V (Grade 5) titanium powder for the M.A.T. multi-head extrusion printer. Print the green part on a standard FFF head, then debind and sinter to a dense, high-strength, lightweight titanium component.
Why engineers choose Fila-MAT Titanium
Four things a process engineer checks before qualifying a bound-metal feedstock.
844 MPa yield, 940 MPa tensile
Rp0.2 844 MPa / Rm 940 MPa post-sinter, tested to ASTM E8/E8M — Ti6Al4V (Grade 5) performance, not a filament-vendor estimate.
4.33 g/cc — lightweight alloy
Low-density titanium at 4.33 g/cc — high strength-to-weight for aerospace and lightweight structures.
Tested at ESA’s ESTEC facility
Mechanical data measured with calibrated equipment at the European Space Agency’s technology centre in the Netherlands — third-party test conditions.
Debind & sinter parameters included
Every spool ships with 3DCeram’s datasheet and process parameters for the M.A.T. FFF head, so green parts reach target density predictably.
How the Fila-MAT workflow runs
Print, debind, sinter — the same three-step process behind every bound-metal FFF part.
Print on the M.A.T. FFF head
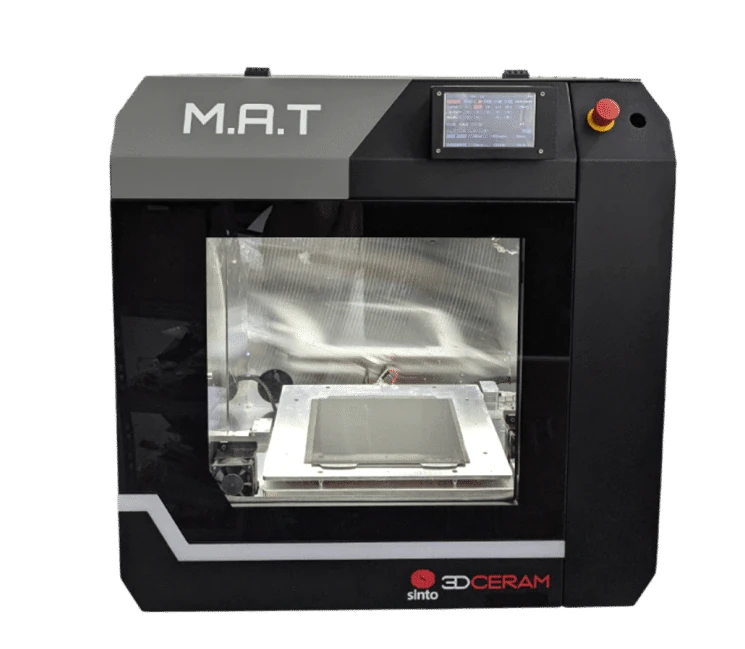
1.75mm feedstock runs on 3DCeram’s M.A.T. printer — max nozzle 270°C, max bed 110°C, with heated filament and print chambers for consistent extrusion.
Debind the binder
Binder-removal parameters ship with every spool’s datasheet, tuned for the titanium feedstock — no trial-and-error on the first batch.
Sinter to dense metal
High-temperature sintering consolidates the part to dense Ti6Al4V — ready for use or optional stress-relief.
Material properties (post-sinter)
| Property | Value | Standard |
|---|---|---|
| Density | 4.33 g/cc | — |
| Yield strength, Rp0.2 | 844 MPa | ASTM E8/E8M |
| Ultimate tensile strength, Rm | 940 MPa | ASTM E8/E8M |
Tested with calibrated equipment at ESA’s ESTEC technology centre, Netherlands. See the full datasheet in Downloads.
Technical specifications
- Material: Ti6Al4V (Grade 5) titanium alloy, bound-metal FFF feedstock
- Filament diameter: 1.75mm
- Compatible platform: 3DCeram M.A.T. — FFF head, max nozzle 270°C, max bed 110°C, filament chamber ≤50°C, print chamber ≤50–60°C
- Post-processing required: chemical/thermal debind + sinter furnace — parameters supplied with the datasheet on every order
Typical applications
Where teams run Fila-MAT Titanium today.
Not sure Fila-MAT Titanium is the right fit?
Three reasons teams pick a different feedstock or platform — tap the closest match.
Why source Fila-MAT through Additive Plus
- 3DCeram-qualified feedstock for the M.A.T. FFF head — matched to the machine, not a generic substitute.
- Debind and sinter parameters plus full datasheet included with every order.
- Materials engineer on the line for shrinkage, warpage, and heat-treatment questions — NDA standard.
- Custom alloy or ceramic feedstock sourced and qualified on request, typical lead 3–4 weeks.
| Brand | 3DCeram |
| Printing Materials | Metal Filaments |
| Technology | FFF |
| Application | Composite Tooling, Engineering, Jigs & Fixtures, Manufacturing |
Product videos
We source and qualify. Custom feedstock on request.
Need a specific bound-metal or ceramic filament, or parameters for a printer we don't list yet? Our materials team qualifies the feedstock and verifies sinter behavior before you commit. Typical lead 3–4 weeks.
Complete the workflow
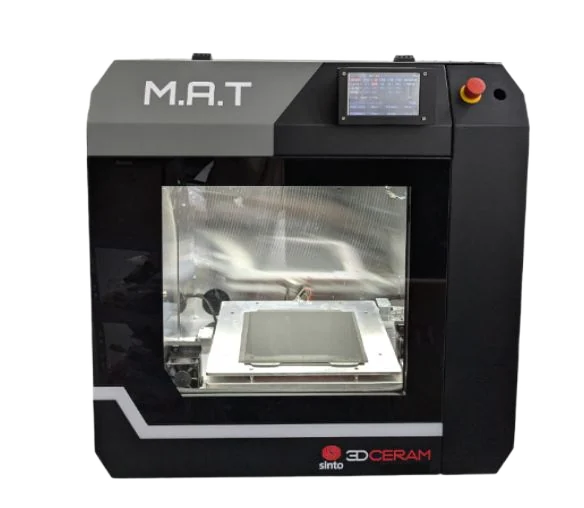
Metal & technical ceramics, printed by extrusion — even silicon carbide.
- FFF · pellet · paste + 3-axis CNC in one machine
- No laser, no loose powder — lab-safe, single-phase
- Official 3DCeram US representative · 12-mo warranty
From $63,000 · Core: FFF + CNC (add Pellet/Paste heads) · made to order, ~3-month build · leasing available
Request a quote Installation and commissioning in the USA: facility and gas planning, start-up and operator training by our US service team.
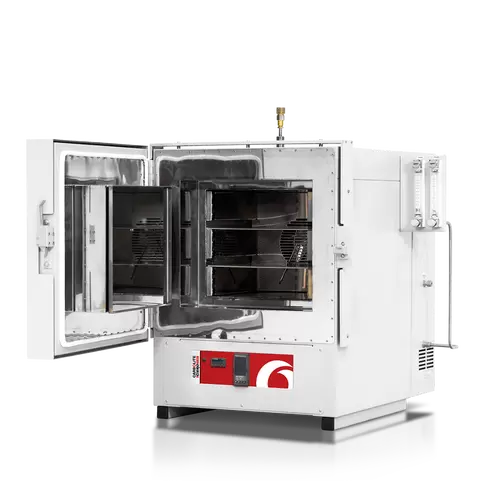
Controlled atmosphere oven for metal AM post-processing and materials research — 400–700°C max (4 grades), 28–1,000 L chambers (5 sizes), O₂ down to 50 ppm with N₂/Ar purge. Seam-welded gas-tight chamber built as an atmosphere unit from the ground up.
- ✓ O₂ down to 50 ppm — atmosphere-controlled heat treatment without vacuum-furnace cost
- ✓ 17 configurations in one family — 28 L lab to 1,000 L production, same gas architecture
- ✓ Seam-welded gas-tight chamber — purpose-built, not a retort-converted standard oven
- ✓ Configured to order — request lead time; install, training & cycle validation included
- ✔ Rp0.2 680 MPa / Rm 880 MPa / 257 HV10 — tested to DIN EN ISO 6892 & 6507-1 at ESA's ESTEC facility
- ✔ Debind & sinter parameters plus full datasheet included with every spool
- ✔ 1.75mm bound-metal feedstock for the 3DCeram M.A.T. FFF head — mutual NDA before any spec review
Other products teams run alongside Fila-MAT Metal Titanium 1,75mm
- ✔ Excellent hot hardness and wear resistance, heat-treatable
- ✔ Print → debind → sinter — great for tooling, dies and inserts
- ✔ Genuine Zetamix by Nanoe · 500 g spool · lead time 10–20 business days (depending on order queue)
In stock
· Ships in 1–2 business days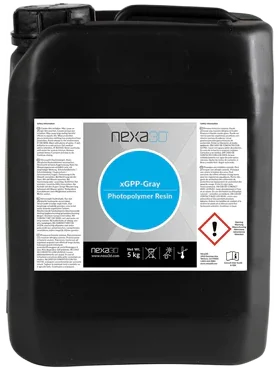
General Purpose Photopolymer (GPP) for high-throughput, high-accuracy production and prototyping on the Nexa3D NXE 400 and NXE 400 Pro. BASF-formulated for injection-mould-quality surface finish, low shrinkage and fast print speed, with 30 MPa ultimate tensile strength, 2100 MPa tensile modulus, 84 D Shore hardness and a 93 °C glass transition. The gray finish shows draft lines, parting seams and surface defects that clear resins hide. Supplied to order in 5 kg (12 lb) jerricans.
Made to order
· Contact for lead time
- ✔ High toughness and flexural strength, wear- and corrosion-resistant
- ✔ Print → debind → sinter to dense zirconia on a desktop FFF machine
- ✔ Genuine Zetamix by Nanoe · 500 g spool · lead time 10–20 business days (depending on order queue)
In stock
Easy-to-print all-round industrial resin with excellent rigidity, an HDT of 122 °C and outstanding chemical resistance — for functional prototypes and demanding industrial parts.
- ✓ 92 MPa tensile · 3600 MPa modulus · HDT-B 122 °C — stiff and heat-stable
- ✓ Outstanding chemical resistance (<1% mass gain) & 0.3% water uptake
- ✓ Post-machinable (drill, grind); long-term thermal stability
- ✓ A cost-effective alternative to Loctite IND249 High Temp
Made to order
· Ships in <10 business days
The open-materials cartridge that unlocks third-party and custom resins on your Nexa3D XiP.
- ✓ Works with NexaX Pro to open the XiP materials platform
- ✓ Gravity-fed dispensing with NFC material versioning
- ✓ Validate and manage your own custom resin profiles
Out of stock
· Currently on backorder — contact us for the latest lead time.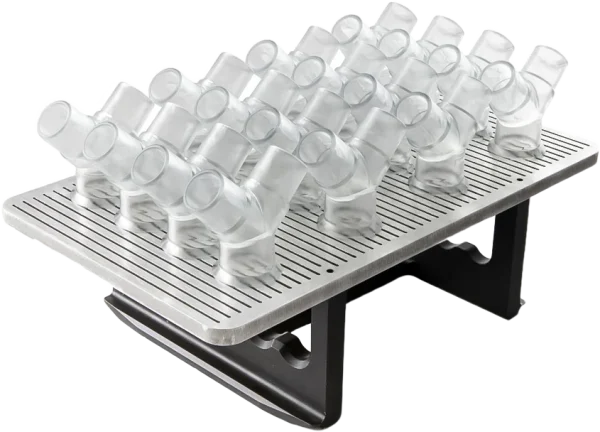
Made to order
· Contact for lead time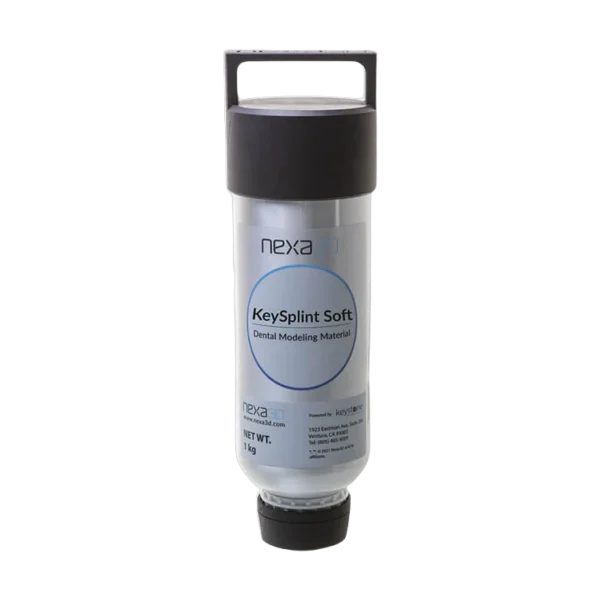
Flexible. Cleared. Comfortable in the mouth. KeySplint Soft prints resilient nightguards, bite planes, splints and repositioners on the Nexa3D XiP desktop printer — FDA 510(k)-cleared and Class IIa biocompatible, with 110% elongation at break so appliances absorb clenching load instead of cracking. Polishes to a clear, patient-ready finish.
Choose your shade: Light Violet or Translucent. 1 kg bottle tuned for XiP, validated print and post-cure profile included.
In stock
· In stock — ships in 1–2 business days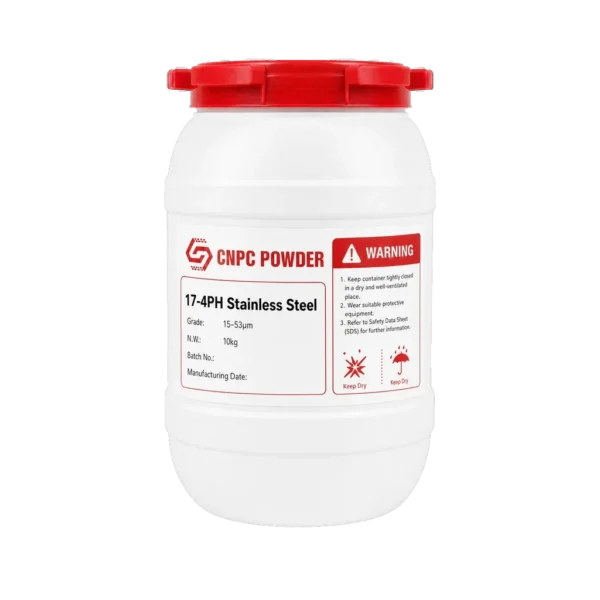
CNPC 17-4PH powder for LPBF — made by CNPC Powder, nitrogen gas-atomized, 15–53 µm, sold in 10 kg containers.
- 10 kg container · $38.50/kg · $385
- Certificate of analysis (COA) for the lot, on request
- Ship date confirmed by email after you order
Manufacturer: CNPC Powder · materials engineer on call · order below or talk to an engineer first.
Made to order
· Ship date confirmed after you orderCommon questions
Don't see yours? Email [email protected] — NDA standard, typical reply within 4 hours.
What is Fila-MAT Metal Titanium and how does it produce metal parts?
Which printer is Fila-MAT Metal Titanium compatible with?
What post-processing does Fila-MAT Metal Titanium require?
What mechanical properties can I expect after sintering?
How much does a Fila-MAT Metal Titanium part shrink during debinding and sintering?
Why print titanium with bound-metal FFF?
Does Fila-MAT Metal Titanium need special sintering?
Place your order, or talk to an engineer first
Order Fila-MAT Metal Titanium 1,75mm direct, or talk to materials engineer