
In stock
- Debind & sinter parameters + datasheet in every order
- Mutual NDA before any file or spec review
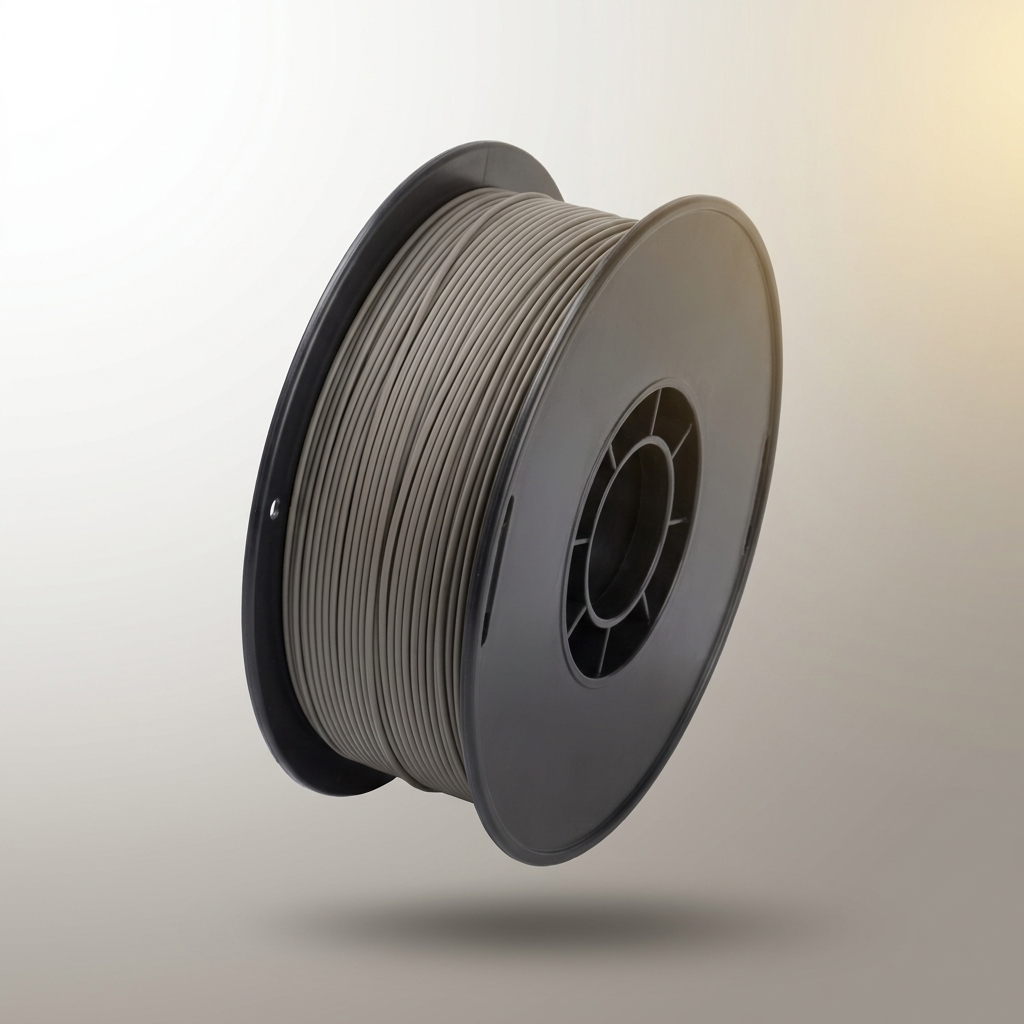
Zetamix 316L Steel Filament 1,75mm
- ✔ Excellent corrosion resistance, ductile and well suited to functional parts
- ✔ Print → debind → sinter to dense 316L on a desktop FFF printer
- ✔ Genuine Zetamix by Nanoe · 500 g spool · lead time 10–20 business days (depending on order queue)
$420
What your process engineer actually checks
Green part to fully dense, predictably
Every spool ships with a datasheet and validated debind/sinter parameters, so green parts reach target density with predictable shrinkage. Lock the cycle once, reorder the same feedstock.
A materials engineer on the line
Questions on debind schedules, sinter shrinkage, density, or warpage on bound-metal/ceramic FFF? A materials engineer answers directly — not a contact-form bot. Most replies in under 4 hours, NDA standard.
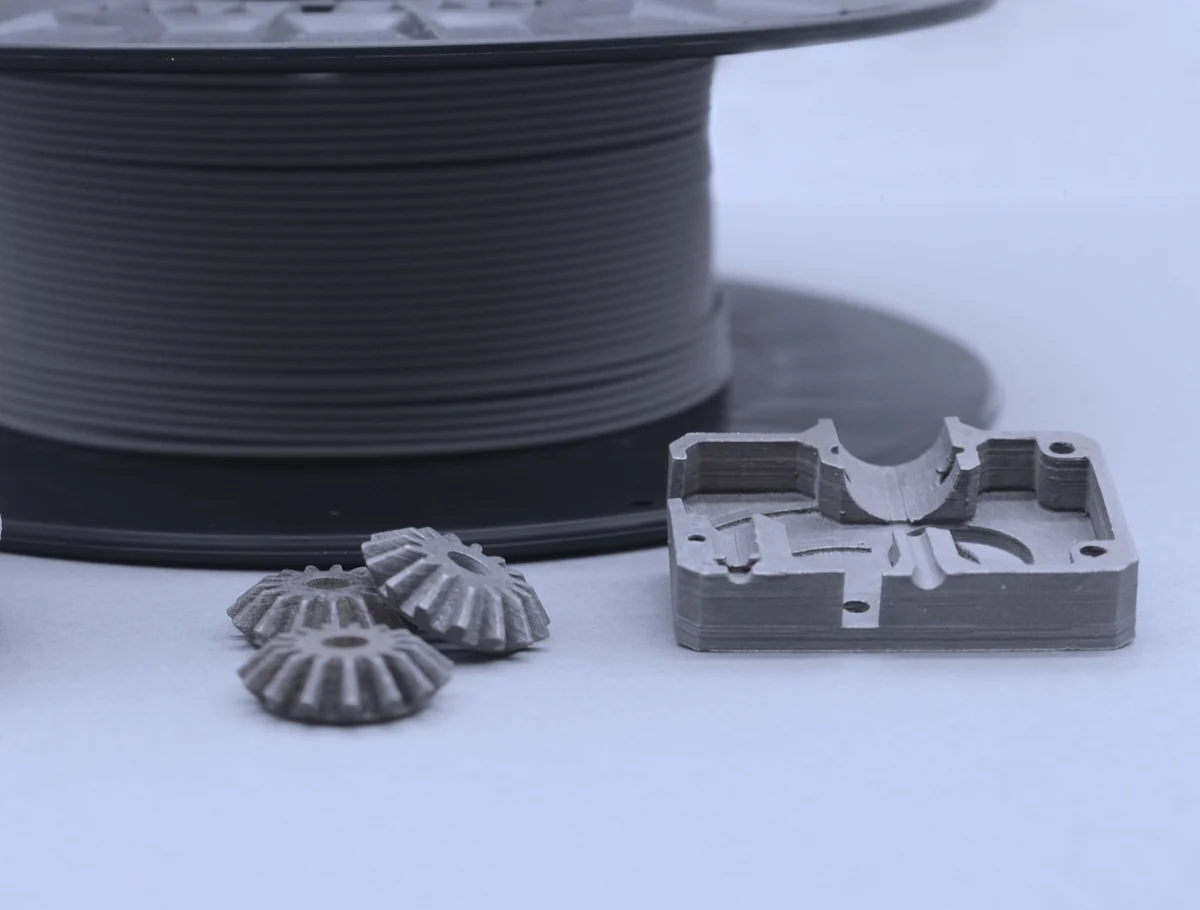
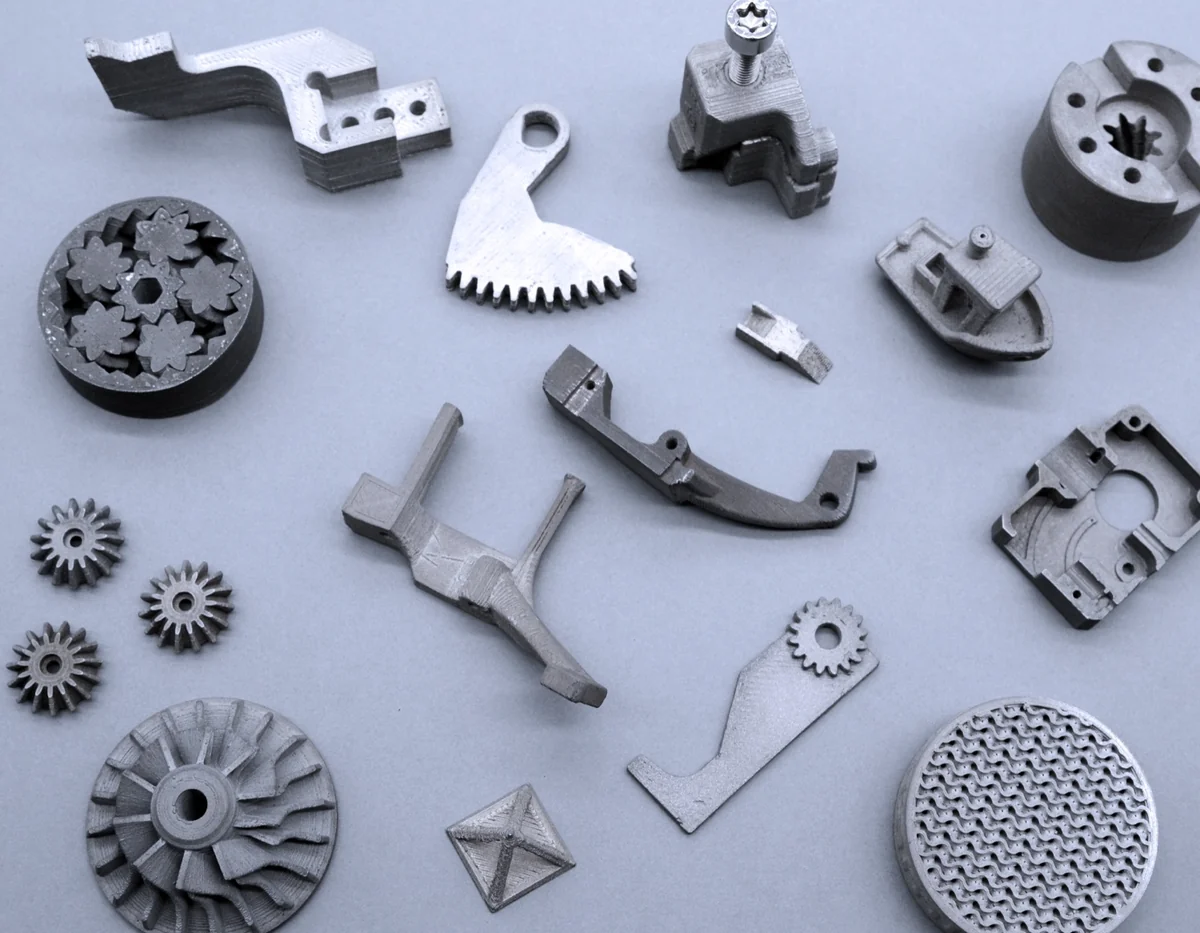
Zetamix 316L stainless steel filament lets you 3D-print functional 316L parts on a standard FFF printer, then debind and sinter to a dense, corrosion-resistant metal component — the same print → debind → sinter workflow we run in-house on our 3DCeram M.A.T.
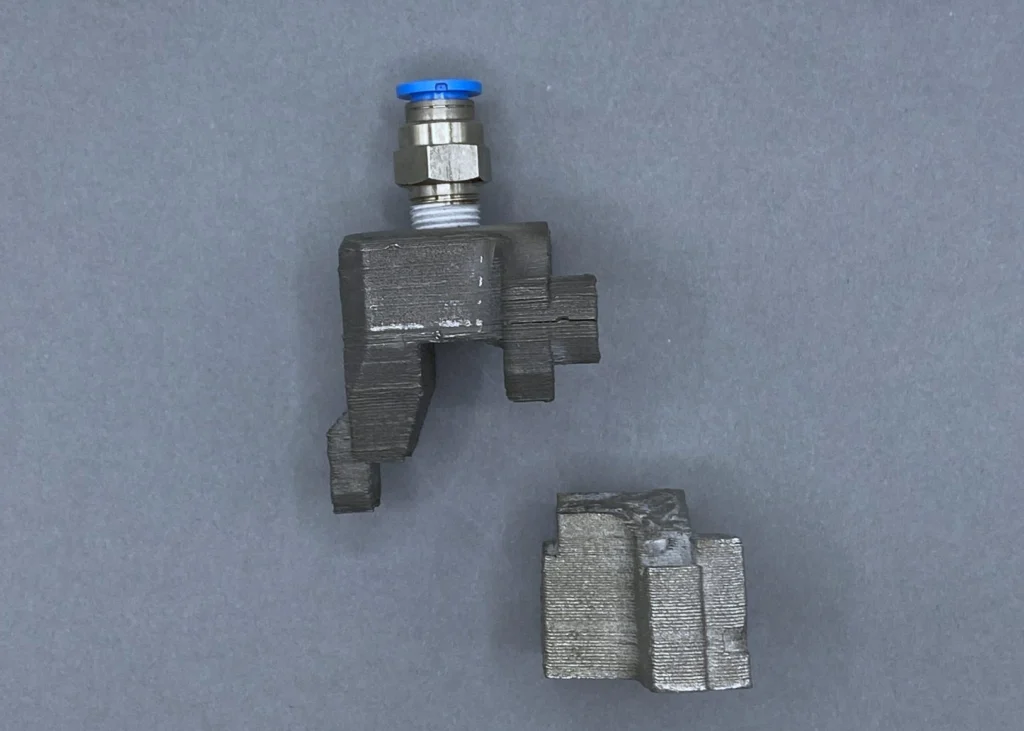
Why engineers choose Zetamix 316L Stainless Steel filament
Authentic 316L stainless steel from a standard FFF printer — ductile, tough and corrosion-resistant after sintering.
Real 316L stainless steel — roughly 92% metal by mass in the filament, sintered to a dense metal part with genuine 316L chemistry.
Resists acids, chlorides and saline environments — for fluid-system parts and components that run in aggressive conditions.
Metal, not brittle ceramic — 316L takes load, bends and absorbs impact where technical ceramics would crack.
Known shrinkage and a defined debind and sinter cycle give predictable, repeatable parts from one print run to the next.
316L stainless steel material properties after sintering
- Composition: authentic 316L stainless steel (~92% metal by mass in the filament)
- Density after sintering: >90% of theoretical
- Corrosion resistance: acids, chlorides and saline environments
- Mechanical character: ductile and tough — metal, not brittle ceramic
- Linear scale for sintering: 118.2% (X/Y) & 117.2% (Z)
- Filament: 1.75 mm
Full specifications are listed in the Specifications tab. Mechanical values are process-dependent — final properties vary with print, debind and sinter parameters.
From spool to dense 316L part
Three stages — the same workflow we run in-house.
Design & scale
Scale the model by 118.2% (X/Y) and 117.2% (Z) for sintering shrinkage. Minimum wall 1 mm, minimum hole 1.5 mm, minimum pin 3 mm, overhangs up to 35° unsupported.
Print on FFF
Print the green part on any standard FFF machine with a grooved drive gear and flexible build plate. Hold a consistent extrusion around 120–130 °C, 3 wall layers minimum.
Debind & sinter
Chemical debind 24 h in acetone at 40 °C, thermal debind at 10 °C/h from 50 to 650 °C in Ar/H₂, then sinter at 50 °C/h to 1350 °C with a 2 h hold in a controlled atmosphere. No furnace? We run this for you.
Where 316L stainless steel is used
Shops 3D-print 316L with Zetamix when they need functional, corrosion-resistant metal parts without machining or tooling.
See real builds in our Zetamix case studies →
No sintering furnace or debinding station? Talk to our team — we’ll help you get set up. Get in touch →
See Zetamix 316L in action
Watch how Zetamix ceramic and metal filaments go from spool to dense, sintered part — the same FFF print → debind → sinter workflow we run in-house.
Choose your Zetamix material
Every Zetamix filament prints on a standard FFF 3D printer — we print and validate them in-house on our 3DCeram M.A.T. system — then debind and sinter to a dense ceramic or metal part. The highlighted row is the material on this page; compare the range below:
| Material | Type | Stands out for | Best for | From |
|---|---|---|---|---|
| Alumina | Technical ceramic | Electrical insulation, ~1550°C | Insulators, high-temp tooling | $495 |
| White Zirconia | Technical ceramic | Toughness & flexural strength | Wear & structural parts | $485 |
| Black Zirconia | Technical ceramic | Zirconia strength, black finish | Aesthetic + technical parts | $550 |
| Silicon Carbide | Technical ceramic | Extreme hardness & thermal | Abrasive / high-temp parts | $550 |
| Porcelain | Ceramic (art) | Glazeable, classic finish | Art, tableware, decorative | $225 |
| 316L | Stainless steel | Corrosion resistance, ductile | Functional metal parts | $420 |
| 17-4 PH | Stainless steel | High strength, hardenable | Tooling & functional parts | $420 |
| H13 | Tool steel | Hot hardness & wear | Dies, inserts, tooling | $420 |
| TiO2 | Specialty ceramic | Specialty technical ceramic | Niche functional parts | $550 |
| Brand | Zetamix by Nanoe |
| Printing Materials | Metal Filaments |
| Technology | FFF |
| Application | Composite Tooling, Engineering, Jigs & Fixtures, Manufacturing |
We source and qualify. Custom feedstock on request.
Need a specific bound-metal or ceramic filament, or parameters for a printer we don't list yet? Our materials team qualifies the feedstock and verifies sinter behavior before you commit. Typical lead 3–4 weeks.
Other products teams run alongside Zetamix 316L Steel Filament 1,75mm
Print radiofrequency parts directly — no debinding, no sintering. A dielectric filament with permittivity 2.2 and low loss, so antennas, lenses and metasurfaces come off the printer ready to test.
- ✔ Permittivity 2.2 · loss tangent 0.001 · HDT up to 110 °C
- ✔ No debinding, no sintering — prints as a technical polymer, parts up to 80 cm
- ✔ Genuine Zetamix by Nanoe · 500 g spool, vacuum packed · 1.75 mm
In stock
· Ships from California · 10–20 business days
xMODEL17-Clear is a high-clarity prototyping resin from Nexa3D — fine feature detail and transparency at very high print speed.
- ✓ High optical clarity for see-through models, fluidics, and light-transmitting prototypes
- ✓ Fine feature resolution with fast throughput on the Nexa3D XiP
- ✓ Genuine Nexa3D resin for the XiP · 1.5 kg · ships from US stock in 2 business days
In stock
· 2 Business Days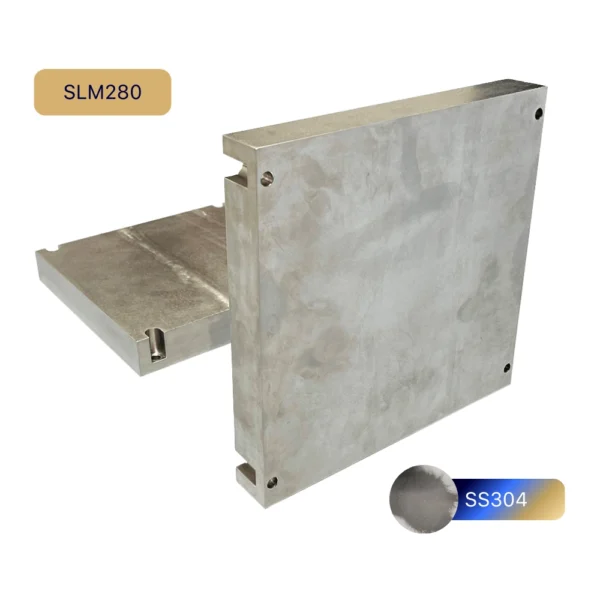
The SLM 280 SS304 Build Platform is a precision-ground stainless steel build plate engineered for reliable LPBF production. Manufactured from high-grade 304 stainless steel and designed as a direct OEM-compatible solution, this SLM 280 metal build plate delivers excellent flatness, thermal stability, and repeatable first-layer performance for industrial additive manufacturing.
Need a custom steel build platform for another printer or alternative thickness? Request a custom quote — we manufacture precision stainless steel and specialty alloy build plates for most industrial LPBF systems.In stock
· Express 2–3 wks · Standard 6–8 wks
Fast, dimensionally stable resin for dental and orthodontic models on the XiP.
- ✓ Crisp detail and stable dimensions for aligner and restorative models
- ✓ Trims and scans cleanly for lab workflows
- ✓ 1 kg cartridge for Nexa3D XiP and XiP Pro (LSPc)
In stock
· 2 Business Days
In stock
· 2 Business Days
Carbon-fiber-reinforced PET filament for FDM 3D printing — high strength (87 MPa tensile) and stiffness (6025 MPa modulus) with excellent dimensional stability, for structural brackets, tooling, and end-use parts under load.
- ✓ ±0.02mm diameter tolerance — consistent extrusion, low jam risk
- ✓ Validated print profile + datasheet included
- ✓ In stock, ships in 1–2 business days
In stock
In stock
In stock
· In stock — ships in 1–2 business days from our Los Angeles warehouse.Common questions
Don't see yours? Email [email protected] — NDA standard, typical reply within 4 hours.
What equipment do I need beyond my 3D printer?
How do the mechanical properties compare to traditional 316L?
What are the design limitations?
What safety precautions are required?
Can I create food-safe or medical components?
How long does the complete process take?
What's the shelf life and storage requirements?
What applications is this best suited for?
Can I use supports and how are they removed?
Place your order, or talk to an engineer first
Order Zetamix 316L Steel Filament 1,75mm direct, or talk to materials engineer