
In stock
- Debind & sinter parameters + datasheet in every order
- Mutual NDA before any file or spec review
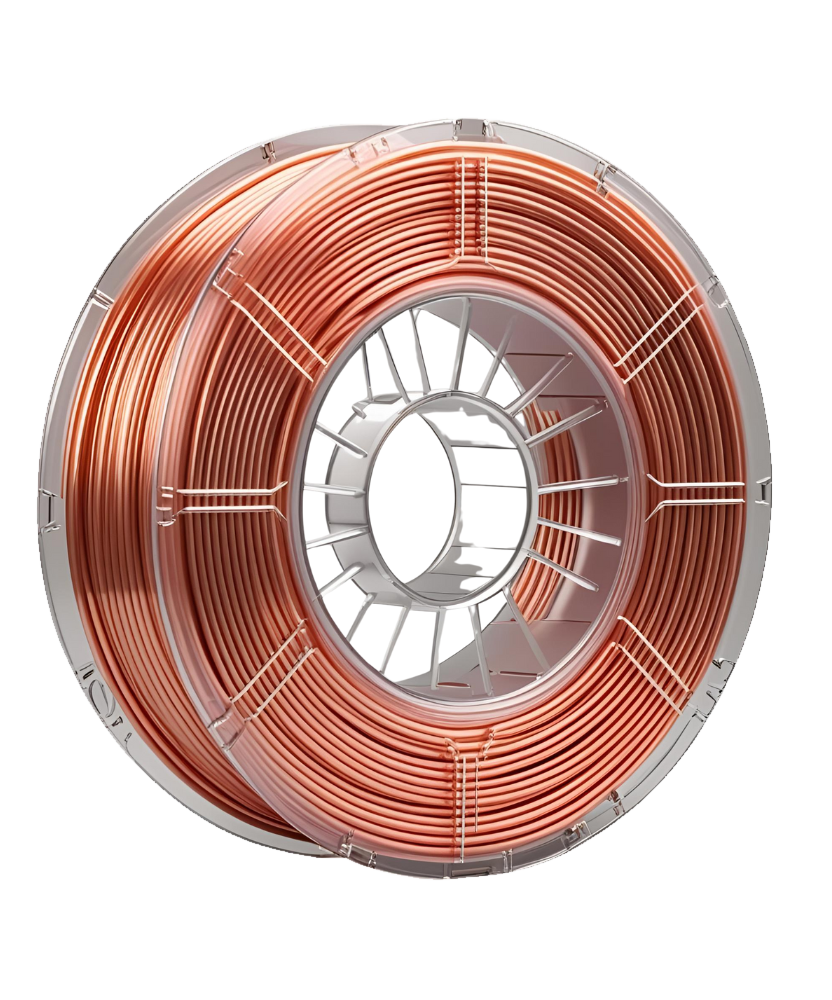
Fila-MAT Metal Copper 1,75mm
Print pure-copper parts on 3DCeram's M.A.T. FFF platform, then debind and sinter to dense, thermally and electrically conductive metal.
- ✔ 228 W/m-K thermal conductivity, 8.4 g/cc density and 118 GPa modulus after sintering
- ✔ Debind and sinter parameters plus the full datasheet included with every spool
- ✔ 1.75mm bound-metal feedstock for the 3DCeram M.A.T. FFF head — mutual NDA before any spec review
What your process engineer actually checks
Conductivity you can design to
228 W/m-K thermal conductivity, 8.4 g/cc density and a 118 GPa modulus after sintering — the reason teams reach for copper in heat exchangers, inductors and thermal-management parts. Measured values on the datasheet, not a filament-vendor estimate.
Debind and sinter parameters included
Every spool ships with 3DCeram's datasheet and the full print, debind and sinter cycle for the M.A.T. FFF head, so green parts reach target density on the first build instead of after trial-and-error.
A materials engineer on the line
Shrinkage, density and sintering questions go to an engineer who has run bound-metal FFF — not a ticket queue. Sub-4h reply, mutual NDA standard before any spec review.
.tabs-section .tab-pane table{border-collapse:separate;border-spacing:0;width:100%;border:1px solid #E6E8EC;border-radius:12px;overflow:hidden;margin:18px 0;font-size:15px;line-height:1.45}.tabs-section .tab-pane table th,.tabs-section .tab-pane table td{border-bottom:1px solid #EFF1F4;border-right:1px solid #EFF1F4;padding:11px 14px;text-align:left;vertical-align:top;color:#23262B}.tabs-section .tab-pane table thead th{background:#F4F1E9;color:#1C2A3A;border-bottom:2px solid #D6B16F;font-weight:700;letter-spacing:.02em}.tabs-section .tab-pane table tbody th,.tabs-section .tab-pane table tbody td:first-child{background:#F7F8FA;font-weight:600;color:#101114}.tabs-section .tab-pane table tr td:last-child,.tabs-section .tab-pane table tr th:last-child{border-right:0}.tabs-section .tab-pane table tbody tr:last-child td{border-bottom:0}.tabs-section .tab-pane h2{border-left:3px solid #D6B16F;padding-left:12px;margin-top:30px}.tabs-section .tab-pane ul{list-style:square;padding-left:20px}.tabs-section .tab-pane ul li::marker{color:#D6B16F}.final-cta{display:none}.rev-section{display:none!important}.tabs-section .tab-pane figure{margin:24px auto;text-align:center;max-width:600px}.tabs-section .tab-pane figure img{max-width:600px;width:100%;height:auto;border-radius:14px;border:1px solid #F0EDE8}.tabs-section .tab-pane figcaption{font-size:12.5px;color:#8C877D;margin-top:7px}
.tab-pane .lead{font-size:15.5px;color:#5B5751;line-height:1.6;max-width:820px}
.tab-pane .desc-block{margin-top:32px}
.tab-pane .desc-block-head{margin-bottom:14px;max-width:780px}
.tab-pane .desc-block-head h4{font-size:17px;font-weight:800;letter-spacing:-.01em;color:#323131;margin:0 0 4px;position:relative;padding-left:14px}
.tab-pane .desc-block-head h4::before{content:””;position:absolute;left:0;top:5px;bottom:5px;width:3px;border-radius:2px;background:#D6B16F}
.tab-pane .desc-block-head .sub{font-size:13px;color:#8C877D;line-height:1.55;margin:0;padding-left:14px}
.tab-pane .tbl-note{font-size:12px;color:#8C877D;margin-top:-8px}
.tab-pane .feat-grid{display:grid;grid-template-columns:repeat(2,1fr);gap:14px 28px;margin-top:8px;padding-left:14px}
.tab-pane .feat-grid br,.tab-pane .app-chips br,.tab-pane .alt-grid br,.tab-pane .how-grid br{display:none}
.tab-pane .feat-tile{display:flex;gap:11px;align-items:flex-start}
.tab-pane .feat-tile .ft-ico{width:26px;height:26px;border-radius:6px;background:#FBF9F4;color:#5B5751;display:flex;align-items:center;justify-content:center;flex-shrink:0;margin-top:1px;border:1px solid #F0EDE8}
.tab-pane .feat-tile .ft-ico svg{width:14px;height:14px;fill:currentColor}
.tab-pane .feat-tile h5{font-size:13.5px;font-weight:700;color:#323131;margin:0 0 2px;line-height:1.3}
.tab-pane .feat-tile p{font-size:12.5px;color:#5B5751;line-height:1.5;margin:0}
.tab-pane .how-grid{display:grid;grid-template-columns:repeat(3,1fr);gap:24px;margin-top:8px;padding:22px 24px;background:linear-gradient(135deg,#070F22 0%,#0B1B3A 50%,#2D2A22 100%);border-radius:12px;position:relative;overflow:hidden;color:#fff}
.tab-pane .how-grid::before{content:””;position:absolute;top:0;left:0;right:0;height:3px;background:linear-gradient(90deg,#D6B16F 0%,#FFE2A6 50%,#D6B16F 100%)}
.tab-pane .how-step{position:relative;z-index:1}
.tab-pane .how-step .hs-n{font-family:”SF Mono”,ui-monospace,monospace;font-size:10px;font-weight:700;color:#D6B16F;letter-spacing:.1em;margin-bottom:6px;display:inline-flex;align-items:center;gap:6px;text-transform:uppercase}
.tab-pane .how-step .hs-n::before{content:””;width:14px;height:1px;background:#D6B16F}
.tab-pane .how-step h6{font-size:13.5px;font-weight:800;color:#fff;margin:0 0 4px;line-height:1.25}
.tab-pane .how-step p{font-size:12.5px;color:rgba(255,255,255,.78);line-height:1.5;margin:0}
.tab-pane .app-chips{display:grid;grid-template-columns:repeat(2,1fr);gap:9px 28px;margin-top:8px;padding-left:14px}
.tab-pane .app-chip{display:flex;align-items:center;gap:10px}
.tab-pane .app-chip .ac-ico{width:22px;height:22px;border-radius:5px;background:#FBF9F4;color:#5B5751;display:flex;align-items:center;justify-content:center;flex-shrink:0;border:1px solid #F0EDE8}
.tab-pane .app-chip .ac-ico svg{width:12px;height:12px;fill:currentColor}
.tab-pane .app-chip .ac-t{font-size:13px;color:#323131;font-weight:700}
.tab-pane .app-chip .ac-s{font-size:11.5px;color:#8C877D;font-weight:500;margin-top:1px}
.tab-pane .alt-grid{display:grid;grid-template-columns:repeat(3,1fr);gap:12px;margin-top:8px}
.tab-pane .alt-card{background:#fff;border:1px solid #EAE7E1;border-radius:10px;padding:14px 16px 13px;display:flex;flex-direction:column;gap:5px;position:relative;overflow:hidden;text-decoration:none;transition:border-color .2s,transform .2s,box-shadow .2s}
.tab-pane .alt-card::before{content:””;position:absolute;top:0;left:0;right:0;height:2px;background:#D6B16F;transform:scaleX(.15);transform-origin:left;transition:transform .3s}
.tab-pane .alt-card:hover{border-color:#D6B16F;transform:translateY(-2px);box-shadow:0 6px 16px rgba(20,16,8,.08)}
.tab-pane .alt-card:hover::before{transform:scaleX(1)}
.tab-pane .alt-card .ac-lbl{font-size:10.5px;font-weight:700;color:#8C877D;letter-spacing:.06em;text-transform:uppercase}
.tab-pane .alt-card .ac-name{font-size:15px;font-weight:800;color:#323131;line-height:1.2}
.tab-pane .alt-card .ac-meta{font-size:11.5px;color:#5B5751;line-height:1.4;margin-top:1px}
.tab-pane .alt-card .ac-cta{margin-top:8px;font-size:12px;color:#5B5751;display:inline-flex;align-items:center;gap:5px;font-weight:600;padding-top:8px;border-top:1px solid #F0EDE8}
.tab-pane .alt-card:hover .ac-cta{color:#323131}
.tab-pane .desc-close{margin-top:16px;padding:15px 20px;background:#FBF9F4;border-left:3px solid #D6B16F;border-radius:0 8px 8px 0;font-size:13.5px;color:#5B5751;line-height:1.55;max-width:820px}
.tab-pane .desc-close b{color:#323131;font-weight:700}
.tab-pane .desc-close .btn-spec{display:inline-flex;align-items:center;gap:7px;margin-top:12px;padding:10px 20px;border:0;border-radius:999px;background:linear-gradient(135deg,#FFBF00,#FF9000);color:#1C1A16;font-weight:700;font-size:13px;cursor:pointer;transition:transform .15s,box-shadow .15s}
.tab-pane .desc-close .btn-spec:hover{transform:translateY(-1px);box-shadow:0 6px 14px rgba(255,144,0,.35)}
@media(max-width:760px){.tab-pane .feat-grid,.tab-pane .app-chips,.tab-pane .alt-grid,.tab-pane .how-grid{grid-template-columns:1fr}}
Fila-MAT Metal Copper is 3DCeram’s bound-metal FFF feedstock — 1.75mm filament loaded with pure copper powder for the M.A.T. multi-head extrusion printer. Print the green part on a standard FFF head, then debind and sinter to a dense, thermally and electrically conductive copper component.
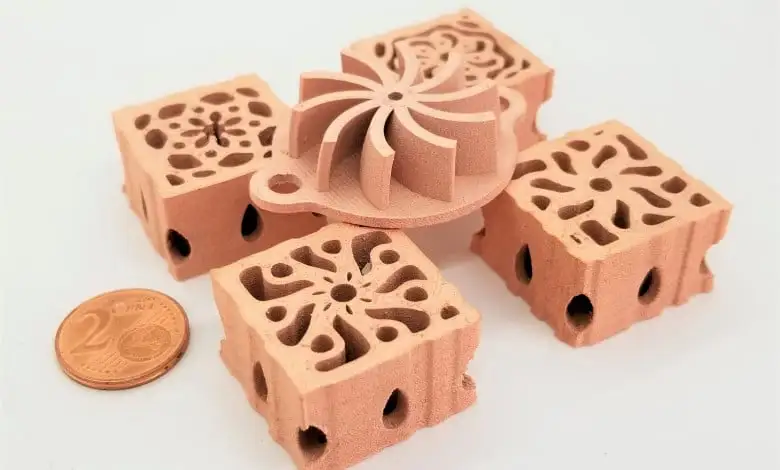
Why engineers choose Fila-MAT Copper
Four things a process engineer checks before qualifying a bound-metal feedstock.
228 W/m-K thermal conductivity
Measured on sintered parts — high-conductivity copper for thermal-management and electrical components, not a filament-vendor estimate.
8.4 g/cc dense copper
Near-full-density copper after sintering, with a 118 GPa elastic modulus (ASTM E8/E8M).
Tested at ESA’s ESTEC facility
Mechanical data measured with calibrated equipment at the European Space Agency’s technology centre in the Netherlands — third-party test conditions.
Debind & sinter parameters included
Every spool ships with 3DCeram’s datasheet and process parameters for the M.A.T. FFF head, so green parts reach target density predictably.
How the Fila-MAT workflow runs
Print, debind, sinter — the same three-step process behind every bound-metal FFF part.
Print on the M.A.T. FFF head
1.75mm feedstock runs on 3DCeram’s M.A.T. printer — max nozzle 270°C, max bed 110°C, with heated filament and print chambers for consistent extrusion.
Debind the binder
Binder-removal parameters ship with every spool’s datasheet, tuned for the copper feedstock — no trial-and-error on the first batch.
Sinter to dense metal
High-temperature sintering consolidates the part to dense, conductive copper — ready to use.
Material properties (post-sinter)
| Property | Value | Standard |
|---|---|---|
| Density | 8.4 g/cc | — |
| Thermal conductivity | 228 W/m-K | — |
| Elastic modulus | 118 GPa | ASTM E8/E8M |
Tested with calibrated equipment at ESA’s ESTEC technology centre, Netherlands. See the full datasheet in Downloads.
Technical specifications
- Material: Pure copper, bound-metal FFF feedstock
- Filament diameter: 1.75mm
- Compatible platform: 3DCeram M.A.T. — FFF head, max nozzle 270°C, max bed 110°C, filament chamber ≤50°C, print chamber ≤50–60°C
- Post-processing required: chemical/thermal debind + sinter furnace — parameters supplied with the datasheet on every order
Typical applications
Where teams run Fila-MAT Copper today.
Not sure Fila-MAT Copper is the right fit?
Three reasons teams pick a different feedstock or platform — tap the closest match.
Why source Fila-MAT through Additive Plus
- 3DCeram-qualified feedstock for the M.A.T. FFF head — matched to the machine, not a generic substitute.
- Debind and sinter parameters plus full datasheet included with every order.
- Materials engineer on the line for shrinkage, warpage, and heat-treatment questions — NDA standard.
- Custom alloy or ceramic feedstock sourced and qualified on request, typical lead 3–4 weeks.
| Brand | 3DCeram |
| Printing Materials | Metal Filaments |
| Technology | FFF |
| Application | Composite Tooling, Engineering, Jigs & Fixtures, Manufacturing |
Product videos
We source and qualify. Custom feedstock on request.
Need a specific bound-metal or ceramic filament, or parameters for a printer we don't list yet? Our materials team qualifies the feedstock and verifies sinter behavior before you commit. Typical lead 3–4 weeks.
Complete the workflow
Metal & technical ceramics, printed by extrusion — even silicon carbide.
- FFF · pellet · paste + 3-axis CNC in one machine
- No laser, no loose powder — lab-safe, single-phase
- Official 3DCeram US representative · 12-mo warranty
From $63,000 · Core: FFF + CNC (add Pellet/Paste heads) · made to order, ~3-month build · leasing available
Request a quote Installation and commissioning in the USA: facility and gas planning, start-up and operator training by our US service team.
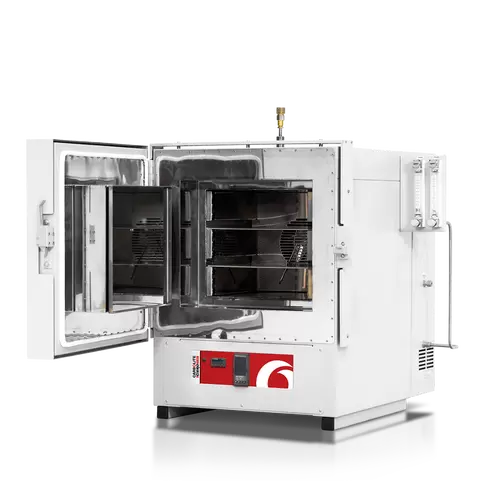
Controlled atmosphere oven for metal AM post-processing and materials research — 400–700°C max (4 grades), 28–1,000 L chambers (5 sizes), O₂ down to 50 ppm with N₂/Ar purge. Seam-welded gas-tight chamber built as an atmosphere unit from the ground up.
- ✓ O₂ down to 50 ppm — atmosphere-controlled heat treatment without vacuum-furnace cost
- ✓ 17 configurations in one family — 28 L lab to 1,000 L production, same gas architecture
- ✓ Seam-welded gas-tight chamber — purpose-built, not a retort-converted standard oven
- ✓ Configured to order — request lead time; install, training & cycle validation included
Print 316L stainless-steel parts on 3DCeram's M.A.T. FFF platform, then debind and sinter to dense, corrosion-resistant metal.
- ✔ Rp0.2 149 MPa, Rm 485 MPa and 158 GPa modulus after sintering — tested to ASTM E8/E8M
- ✔ Debind and sinter parameters plus the full datasheet included with every spool
- ✔ 1.75mm bound-metal feedstock for the 3DCeram M.A.T. FFF head — mutual NDA before any spec review
Other products teams run alongside Fila-MAT Metal Copper 1,75mm
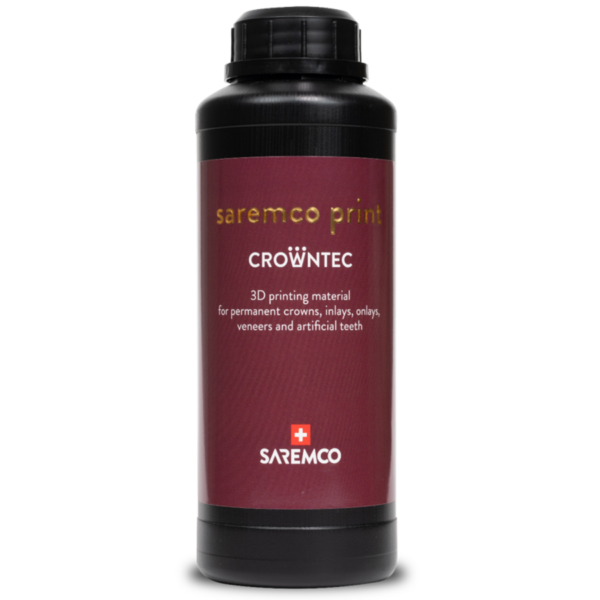
Light-curing filled composite for permanent crowns, inlays, onlays, veneers and denture teeth — shade A2, validated on Nexa3D LSPc.
- ✓ Permanent indication: flexural strength > 130 MPa (ISO 4049), E-modulus > 4000 MPa
- ✓ One-phase esthetics — pre-matched A2 opacity, no layering; biocompatible after UV post-cure
- ✓ 0.5 kg ready-to-use bottle, zero pre-mixing · ships in 1–2 business days
In stock
· 1–2 Business Days
In stock
· 1–2 Business Days
In stock
Print titanium parts on 3DCeram's M.A.T. FFF platform, then debind and sinter to dense, high-strength, lightweight metal.
- ✔ Rp0.2 844 MPa, Rm 940 MPa at 4.33 g/cc after sintering — tested to ASTM E8/E8M
- ✔ Debind and sinter parameters plus the full datasheet included with every spool
- ✔ 1.75mm bound-metal feedstock for the 3DCeram M.A.T. FFF head — mutual NDA before any spec review
In stock
· In stock — ships in 1–2 business days. Custom alloy or ceramic feedstock: 3–4 weeks, configured to order.
Semi-flex matte black resin (HDT60): no post-cure needed for impact-resistant jigs & fixtures
Availability: confirmed at order. Supplier stock for this line varies — we verify availability and lead time on every order before processing, and offer an equivalent or a full refund if an item cannot be supplied. Cubic Ink equivalents →
Made to order
· Available to order — we confirm the lead time by email within one business day of your order.
xPRO410 is a rigid, general-purpose LSPc photopolymer built on Henkel Loctite® PRO410 chemistry — extreme accuracy and an exceptional surface finish, optimized for the Nexa3D NXE 400 at up to 8 L/hour.
- ✓ Rigid general-purpose resin — 41 MPa tensile, Shore D 79
- ✓ Dimensional accuracy within 0.2% after xCURE post-cure
- ✓ 5 kg container for NXE 400 / 400Pro (405 nm LSPc)
- ✓ In stock — ships in 1–2 business days from US inventory
In stock
· In stock — ships in 1–2 business days from US inventory.
Print the pattern, burn it out clean, cast perfect metal. Engineering-grade castable resin for jewelry, dental and investment casting — stocked in Los Angeles.
- Ash-free burnout — no expansion, no cracked molds
- Fine detail: filigree, crowns, micro-features
- Runs on 405 nm LCD/DLP, LSPc and SLA printers
In stock
- ✓ High toughness & thermal-fatigue resistance for die-casting tooling
- ✓ Gas-atomized — COA on request
- ✓ Sold in small, workable volumes
Available to order
· Lead time on requestCommon questions
Don't see yours? Email [email protected] — NDA standard, typical reply within 4 hours.
What is Fila-MAT Metal Copper and how does it produce metal parts?
Which printer is Fila-MAT Metal Copper compatible with?
What post-processing does Fila-MAT Metal Copper require?
What properties can I expect after sintering?
How much does a Fila-MAT Metal Copper part shrink during debinding and sintering?
Why print copper with bound-metal FFF instead of a laser system?
Place your order, or talk to an engineer first
Order Fila-MAT Metal Copper 1,75mm direct, or talk to materials engineer