
In stock
- Solids loading + debind/sinter guidance in every order
- Mutual NDA before any file or spec review
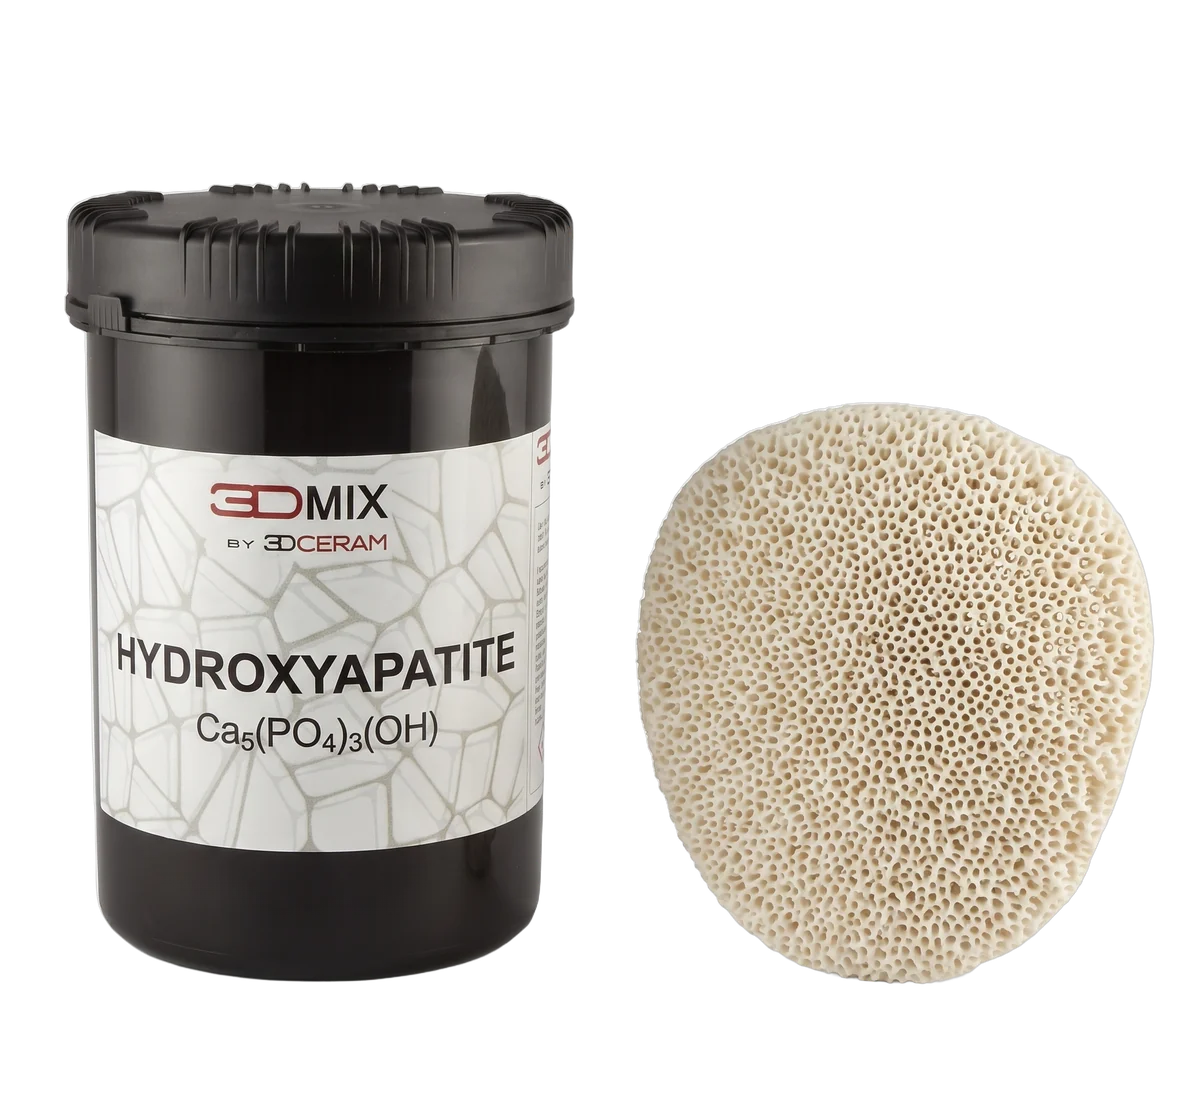
Hydroxyapatite 3D Printing Paste
Print bioactive hydroxyapatite bone-substitute parts on the 3DCeram Ceramaker & M.A.T. ceramic-SLA platforms, then debind and sinter to a clean calcium-phosphate bioceramic.
- ✓ Bioactive calcium phosphate — composition close to bone, crystallinity >95%, heavy metals <30 ppm
- ✓ Print porous, patient-specific implant geometries not possible by machining
- ✓ 55 vol% ceramic load · 405 nm photoinitiator · 250 mL bottle
$1,650
What your regulatory engineer actually checks
Purity and phase data
Crystallinity >95%, Ca/P ratio 1.65–1.82, foreign phases ≥5% and heavy metals <30 ppm — the composition data an implant material must be qualified against. We ship the datasheet.
The full ceramic workflow
Every order ships with the debinding and sintering parameters. Hydroxyapatite is sintered to >96% density, and shrinkage is compensated in build prep so patient-specific geometries land on dimension.
A materials engineer on the line
Bioceramic purity, sintering and qualification are unforgiving. Talk to an engineer who runs this paste — sub-4h reply, NDA standard.
Hydroxyapatite 3D Printing Paste is a 3DCeram hydroxyapatite paste for the Ceramaker laser-SLA platform — a bioactive calcium-phosphate ceramic whose composition is close to natural bone.
Why engineers choose this paste
A bioceramic for bone-substitute and implant work: bioactive, osseointegrating and clean.
Bioactive & osseointegrating
Composition close to bone mineral encourages bone in-growth in orthopaedic and cranial implants.
Controlled purity
Crystallinity >95%, foreign phases ≤5% and heavy metals <30 ppm — specified for biomedical use.
Patient-specific geometry
Print porous, patient-matched implant geometries not possible by machining.
107 MPa bending strength
Sintered structural strength for bone-substitute components.
Print → debind → sinter
Ceramic stereolithography on the 3DCeram Ceramaker platform. The green part is larger than the finished part — shrinkage is compensated in build preparation.
Laser SLA print
The ceramic-loaded paste is cured layer-by-layer on a 3DCeram Ceramaker laser-SLA machine into a green part.
Debinding
The organic binder is removed in a controlled thermal cycle, leaving a fragile ceramic-only brown part.
Sintering
Sintered to >96% dense hydroxyapatite (>1.5 g/cc, ~2 µm grain) with crystallinity above 95%.
Typical applications
Orthopaedic and cranial bone-substitute implants.
Hydroxyapatite — physical & biomedical properties
Representative post-sinter values from the 3DCeram material datasheet. Final numbers depend on part geometry and your qualified sinter cycle. Debinding and shrinkage data are provided for guidance only; print presets are not included — you tune the sinter cycle on your own equipment.
| Property | Value |
|---|---|
| Densification rate | >96% |
| Density | >1.5 g/cm³ |
| Grain size after sintering | 2 µm |
| 4-pt bending strength | 107 MPa |
| Ca/P ratio | 1.65 – 1.82 |
| Foreign phases (CaO, TCP, TTCP) | ≤5% |
| Crystallinity | >95% |
| Heavy metals | <30 ppm |
| Brand | 3DCeram |
| Country of origin | France |
| Printing Materials | Ceramic Pastes |
| Technology | CERAMIC SLA |
| Material | Hydroxyapatite (HA) |
| Application | Dental, Engineering, Jigs & Fixtures, Manufacturing, Medical |
We formulate and qualify. Custom variants on request.
Need a specific ceramic chemistry, solids loading, or a tuned binder for your process? Our materials team formulates and verifies rheology and sinter behavior before you commit. Typical lead 3–4 weeks.
Complete the workflow
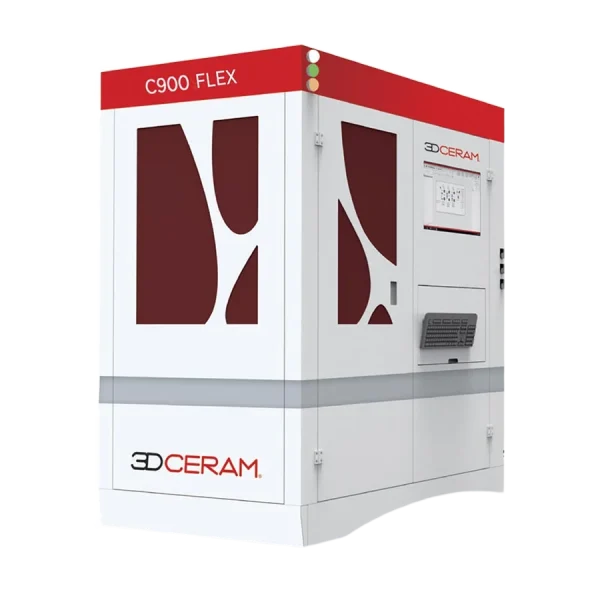
- ✓ 11+ ceramic materials — Al₂O₃, ZrO₂, Si₃N₄, TCP, HA, AlN, cordierite and more
- ✓ Top-down SLA — support-free complex internal geometries in dense ceramic
- ✓ SAM option — 100 mL minimum batch for R&D economy with expensive compositions
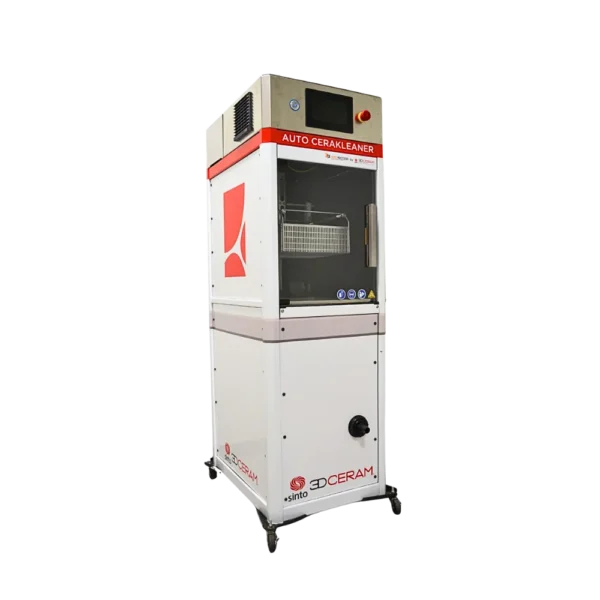
Automated cleaning system that removes excess ceramic paste from freshly printed green parts, leaving them ready to debind — replacing slow, hands-on solvent cleaning in the ceramic AM workflow.
- ✓ Gentle, low-mechanical-stress cleaning of fragile green parts
- ✓ Batch time cut dramatically vs manual (e.g. 60 min → 5 min on 70 alumina parts)
- ✓ Solvent longevity + recycling · no manual solvent contact
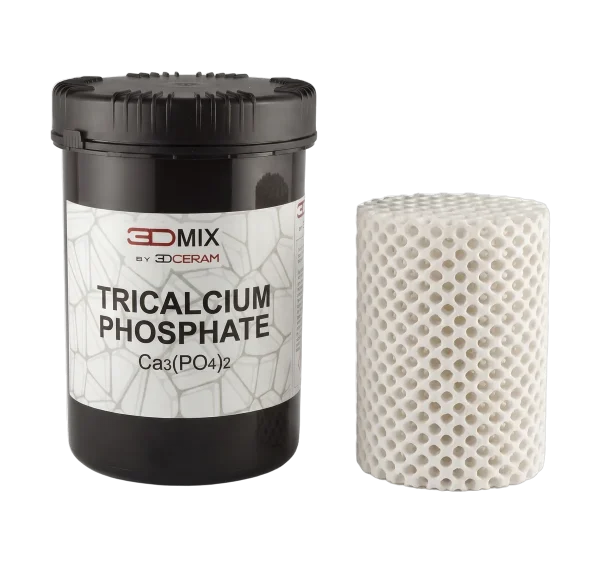
Print bioresorbable tricalcium phosphate (TCP) scaffolds on 3DCeram's Ceramaker laser-SLA platform, then debind and sinter to a clean, resorbable bioceramic.
- ✓ Bioresorbable — gradually replaced by natural bone; Ca/P ratio 1.503, no calcium pyrophosphate
- ✓ Print porous, patient-specific scaffolds for bone regeneration and spinal implants
- ✓ Ceramic SLA paste for the 3DCeram Ceramaker platform — quote-based, mutual NDA before spec review
Other products teams run alongside Hydroxyapatite 3D Printing Paste
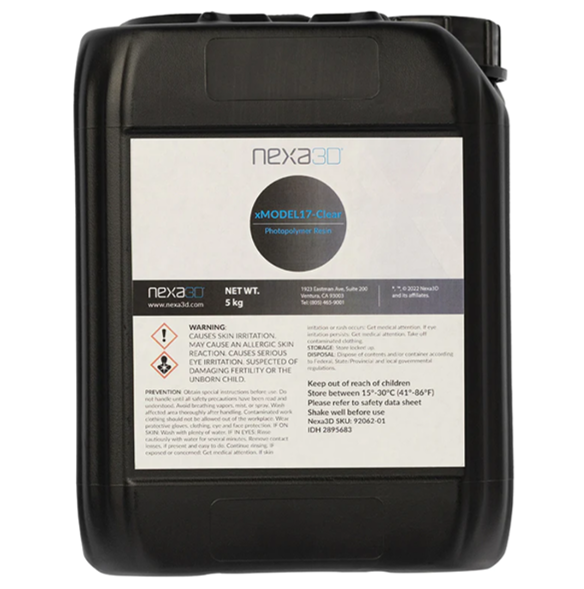
xMODEL17-Clear is a high-clarity prototyping resin from Nexa3D — fine feature detail and transparency at very high print speed.
- ✓ High optical clarity for see-through models, fluidics, and light-transmitting prototypes
- ✓ Fine feature resolution with fast throughput on Nexa3D systems
- ✓ Genuine Nexa3D resin for NXE-series printers · 5 kg · ships from US stock in 2 business days
In stock
· 2 Business Days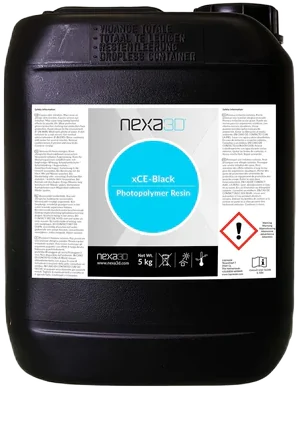
Cyanate-ester-like LSPc resin for stiff, heat-resistant functional parts and injection-molding inserts — 5 kg bottle.
- ✓ 135 MPa flexural strength, 3250 MPa flexural modulus
- ✓ 128 °C glass transition (DMA, E″)
- ✓ Runs on NXE 400/400Pro, XiP and XiP Pro
In stock
· Ships in 1–2 business days from US stock.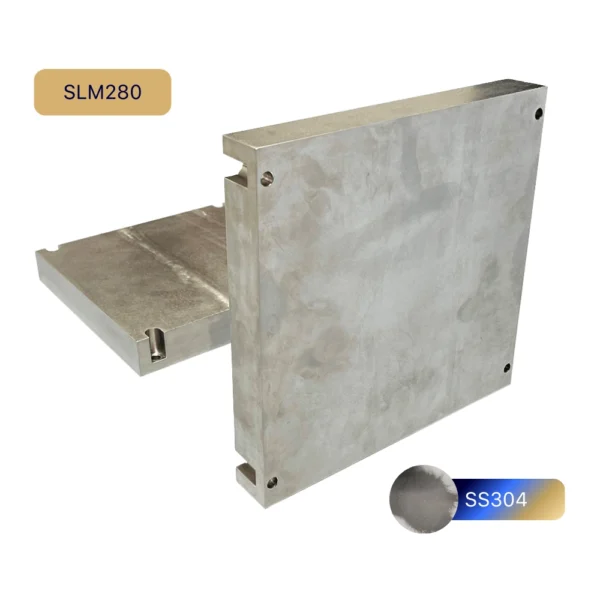
The SLM 280 SS304 Build Platform is a precision-ground stainless steel build plate engineered for reliable LPBF production. Manufactured from high-grade 304 stainless steel and designed as a direct OEM-compatible solution, this SLM 280 metal build plate delivers excellent flatness, thermal stability, and repeatable first-layer performance for industrial additive manufacturing.
Need a custom steel build platform for another printer or alternative thickness? Request a custom quote — we manufacture precision stainless steel and specialty alloy build plates for most industrial LPBF systems.In stock
· Express 2–3 wks · Standard 6–8 wks
Low-viscosity, semi-translucent laser-SLA resin with a 135 °C glass transition — built for prototypes and quick molds that must hold their shape under heat.
- ✓ Tg 135 °C · 87 Shore D · 65 MPa tensile · 110 MPa flexural
- ✓ 340 cps low-viscosity · 0.08–0.12 mm layers on Kings industrial SLA (355 nm)
- ✓ In stock — ships in 1–2 business days from our Los Angeles warehouse
In stock
· In stock — ships in 1–2 business days from our Los Angeles warehouse.
In stock
· 2 Business Days
Strong. Biocompatible. No preliminary cast. KeyTray prints custom individual impression trays straight from the digital scan — Class I biocompatible, with 85 MPa flexural strength and Shore D 86 so the tray survives seating and removal from an undercut without distorting the impression. Compatible with all impression materials; compound waxes and border-molding materials adhere as they would to a conventional tray.
1 kg bottle, translucent blue. Currently out of stock — contact us for the next lot date.
Out of stock
· Out of stock — contact us for the next lot date
Print radiofrequency parts directly — no debinding, no sintering. A dielectric filament with permittivity 4.5 and low loss, so antennas, lenses and metasurfaces come off the printer ready to test.
- ✔ Permittivity 4.5 · loss tangent 0.001 · HDT up to 110 °C
- ✔ No debinding, no sintering — prints as a technical polymer, parts up to 80 cm
- ✔ Genuine Zetamix by Nanoe · 500 g spool, vacuum packed · 1.75 mm
In stock
· Ships from California · 10–20 business days
CNPC Scalmalloy® powder for LPBF — made by CNPC Powder, 20–63 µm, sold in 10 kg containers.
- Certificate of analysis (COA) for the lot, on request
Manufacturer: CNPC Powder
Made to order
· Ship date confirmed after you orderCommon questions
Don't see yours? Email [email protected] — NDA standard, typical reply within 4 hours.
What is Hydroxyapatite and why use it for implants?
How is the material qualified for biomedical use?
How does hydroxyapatite differ from tricalcium phosphate (TCP)?
Why does the printed part shrink during processing?
Can I print porous or patient-specific implants?
Which printer runs this paste, and can I trial it?
Place your order, or talk to an engineer first
Order Hydroxyapatite 3D Printing Paste direct, or talk to materials engineer