
Made to order
- US installation commissioning and operator training included
- Validated parameters a parameter set for your first production alloy
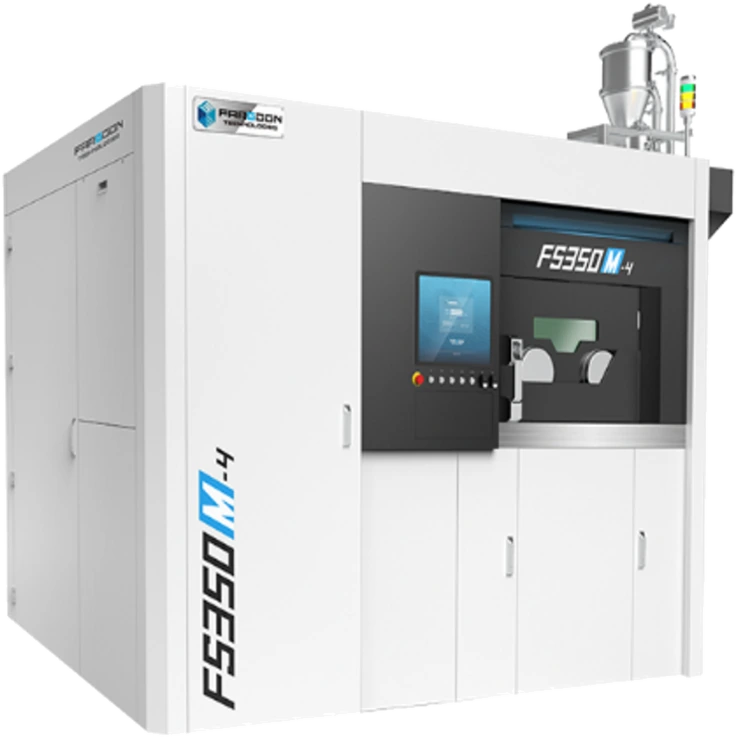
Farsoon FS350M LPBF Metal 3D Printer – 4×500 W, 4×1000 W or 6×500 W Lasers | 17.1×14.1×15.7 in / 433×358×400 mm
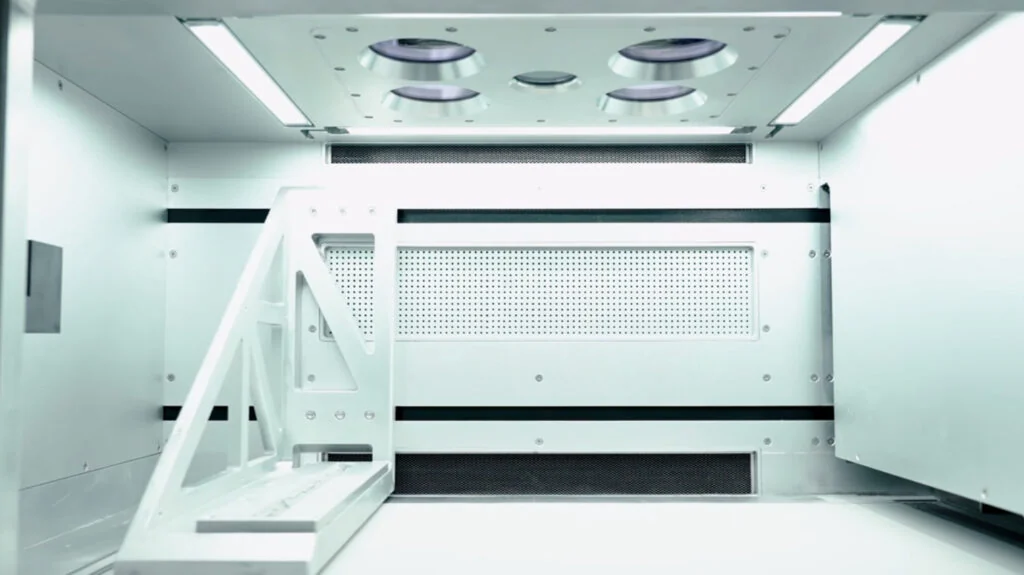
The Farsoon FS350M is a multi-laser LPBF metal 3D printer for medium- to high-volume series production, supplied in 4×500 W, 4×1000 W or 6×500 W laser configurations on the same 17.1×14.1×15.7 in / 433×358×400 mm build cylinder.
- ✓ Three laser configurations — we supply and support all three
- ✓ 17.1×14.1×15.7 in / 433×358×400 mm build on a 65 sq ft / 6 m² class footprint
- ✓ Open platform — full access to process parameters, qualify your own alloy
- ✓ Lead time: built to order — confirmed at quote
Installation and commissioning in the USA: facility and gas planning, start-up and operator training by our US service team.
What your process engineer actually checks
Multi-laser throughput you can verify
Four 500 W, four 1000 W with Beam Shaping, or six 500 W lasers over the same build cylinder. Scanning at up to 32.8 ft/s / 10 m/s, recoating at 400 mm/s, roughly 8 seconds per layer. We hand you the parameter set behind any figure we quote, not just the figure.
An applications engineer on the line
Not a ticket queue — engineers who run LPBF in production in-house at AO Metal. Alloy qualification, parameter development, troubleshooting. Sub-4h reply, NDA standard.
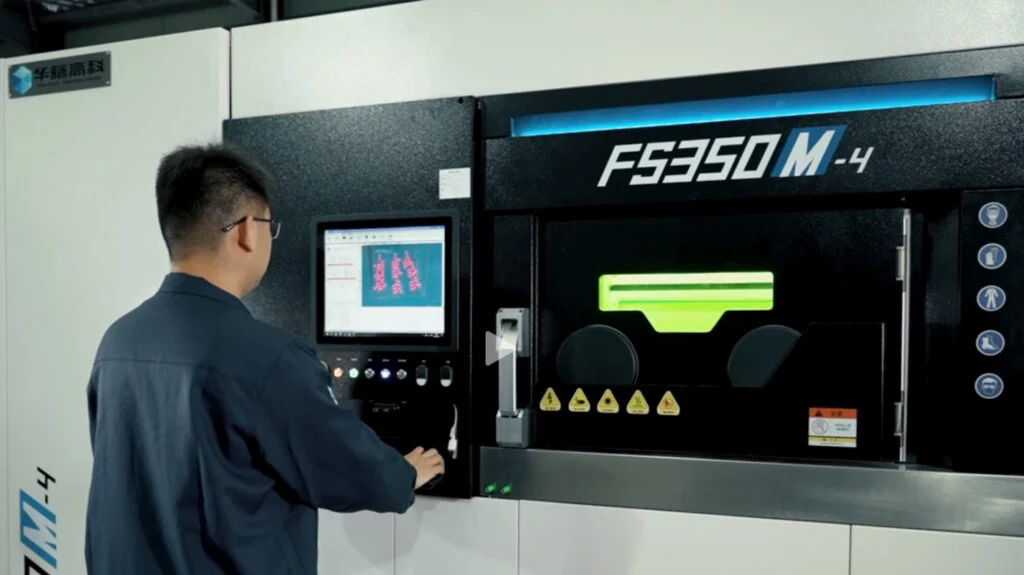
The Farsoon FS350M is a multi-laser LPBF platform for medium- to high-volume metal series production, available in three laser configurations — 4×500 W (FS350M-4), 4×1000 W with Beam Shaping and 6×500 W. All three share the same 17.1×14.1×15.7 in / 433×358×400 mm build cylinder and the same 65 sq ft / 6 m² class footprint, in 316L, AlSi10Mg, Ti6Al4V, 17-4PH, ST1 and Maraging Steel Grade 300.
Why engineers choose the FS350M
Four things your process engineer will check first.
Laser power matched to your part mix
Four 500 W, four 1000 W with Beam Shaping, or six 500 W lasers — same build cylinder either way. Scanning runs at up to 32.8 ft/s / 10 m/s, with recoating at 400 mm/s and roughly 8 seconds per layer.
Truly open platform
Key machine parameters are open. BuildStar and MakeStar allow real-time build parameter modification, so you can qualify an in-house alloy or tune a recipe instead of waiting for a vendor release.
Closed-loop powder management
Sealed supply tank, front glove boxes for breakout, and one shared container for loading, unloading and sieving. Powder stays under argon or nitrogen from delivery through recycling.
Three-stage filtration with back-flush
An integrated three-stage filter module rated for reactive materials. Back-flush extends filter life and cuts the cost of filter changes. Full chamber purge takes 11 minutes; inert gas draw in process is 3–5 L/min.
Three configurations on one platform
Farsoon builds the FS350M in three laser configurations. The build cylinder, the footprint and the powder handling do not change between them — what changes is how much laser you put over the same plate. We supply all three.
| Configuration | Lasers | What it is for |
|---|---|---|
| FS350M-4 | 4 × 500 W | The established baseline, with over 100 systems installed in the consumer products sector alone. The default choice for mixed series production. |
| FS350M 4×1000 W | 4 × 1000 W + Beam Shaping | Double the laser power plus Beam Shaping, which widens the melt pool. Farsoon states up to twice the build efficiency of the 4×500 W configuration, and better support for specialty alloys. |
| FS350M 6×500 W | 6 × 500 W | Developed with industry partners for industrial-scale throughput on serial runs of small to medium parts, where nesting keeps every laser busy. |
Build cylinder 17.1×14.1×15.7 in / 433×358×400 mm and the 6 m² class footprint are the same on all three. Productivity claims are Farsoon's; which configuration pays back on your part mix is the conversation to have before the order.
How we deliver and support it
What happens between the purchase order and your first qualified part.
Pick the configuration, scope the cell
We size the laser count against your part mix and annual volume, then plan power, argon or nitrogen supply and extraction with your facilities team. Footprint is 65 sq ft / 6 m² class with filtration integrated; the US transformer ships with the machine.
Install and train in the USA
Commissioning and operator training by our US service team. First builds are run together, so your operators hand over parts rather than a checklist.
Parameters, spares, engineer
Validated parameter sets for your alloy, US-held spares, and an applications engineer who has run LPBF in production in-house at AO Metal. Sub-4h reply, NDA standard.
What the FS350M is built for
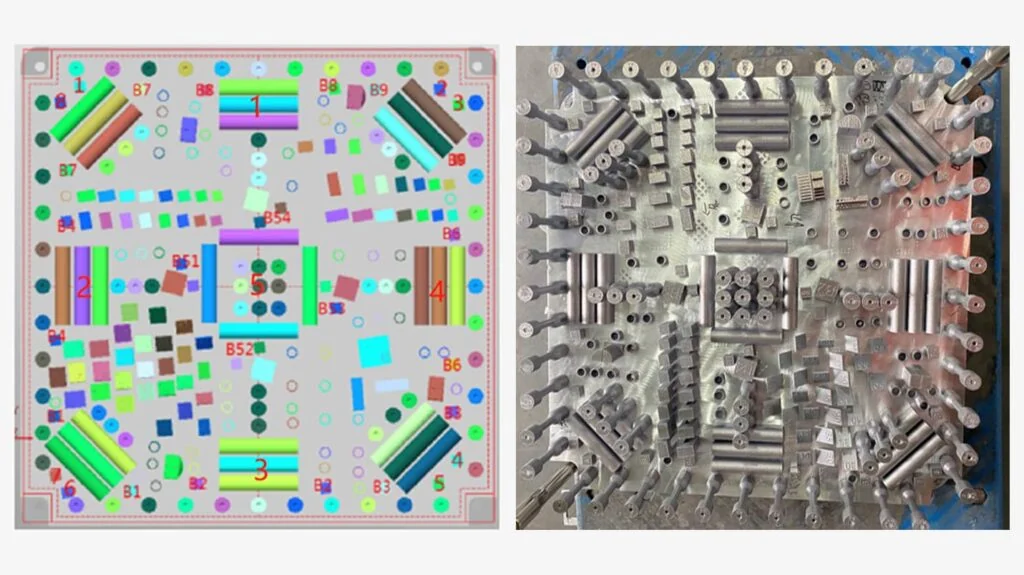
The FS350M-4 ran in serial production at customer sites for close to two years before Farsoon released it to the global market. The platform sits in the range where a part has stopped being a prototype: molds and tooling, automotive and aerospace hardware, and consumer parts produced in repeating batches. Process parameter development — variable layer thickness, adaptive scanning for infill versus detail — is what raises throughput without giving up part quality. Full specifications are in the Specifications tab below.
Build chamber and powder handling
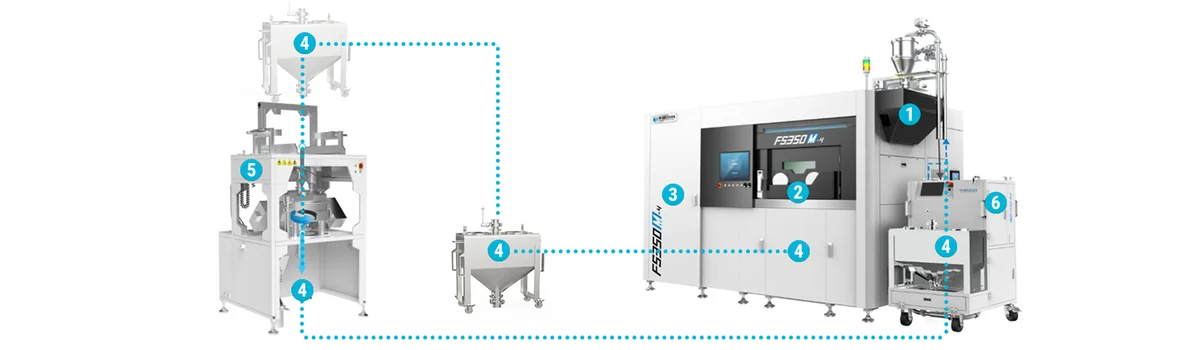
- 1 — Powder supply tank. Connects to the powder delivery unit for fully sealed material delivery under an inert atmosphere, without disturbing the build in progress.
- 2 — Glove box. Sealed glove boxes at the front of the machine allow safe breakout once the build is complete.
- 3 — Integrated filtration system. Three-stage recirculating filter module rated for reactive materials, with a back-flush function that extends filter life.
- 4 — Shared metal container. One container for loading, unloading and sieving, which simplifies powder handling and transport between stations.
- 5 — Sieving unit. A vibration screen filters oversize particles out of recycled powder; refreshed powder goes straight back into supply.
- 6 — Powder delivery unit. A top-feed system tracks powder level in the container and signals a refill; the refill unit docks and tops up material without disturbing the build.
Qualified materials
Farsoon lists 316L, AlSi10Mg, Ti6Al4V, 17-4PH, ST1 and Maraging Steel Grade 300 for the FS350M, with further grades in process development. Because the platform is open, a grade outside that list is a parameter development project rather than a dead end, and one we can run with you. We stock 316L, AlSi10Mg and Ti-6Al-4V in the USA, lot-certified.
Typical applications
Where FS350M systems are actually running.
A production case, in numbers
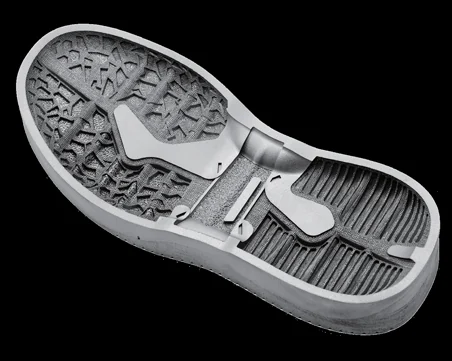
| Shoe mold, 316L, on the FS350M-4 | Figure |
|---|---|
| Part size (each) | 11.4×5.5×1.2 in / 290×140×31 mm |
| Layer thickness | 0.0012 in / 0.03 mm (30 µm) |
| Build time | 24 hours for one pair |
| Coverage | One pair per build covers over 95% of shoe sizes |
Figures as published by Farsoon for this application on the 4×500 W configuration. Build time on your part depends on geometry, nesting and parameter set.
Watch the Farsoon FS350M system showcase →
Not sure the FS350M is the right frame size?
Three Farsoon LPBF platforms either side of it.
Bigger envelopeFarsoon FS422M CAMSView printer →
Large formatFarsoon FS812M-UView printer →
Why source the FS350M through Additive Plus
- All three laser configurations supplied and supported — we help you pick, not just quote.
- US sales, installation, commissioning and operator training by our own service team.
- Applications engineering from a team that runs LPBF in production in-house at AO Metal — parameter development, not a ticket queue.
- Lot-certified metal powders stocked in the USA for the alloys this machine runs.
- Leasing and financing available on capital equipment.
- Print a paid benchmark part in California before you commit to a system.
- Response under 24 hours · 200+ AM systems delivered across 23 countries.
| Brand | Farsoon Technologies |
| External Dimensions (L×W×H) | 128.3×72.8×90.6 in / 3260×1850×2300 mm |
| Build Volume | 433×358×400 mm (17.1×14.1×15.7 in) (Height incl. build plate) |
| Net Weight | Approx. 7275 lb / 3300 kg |
| Layer thickness | 0.02~0.1 mm (0.0008-0.0039 in) |
| Scanning Speed | Max. 32.8 ft/s / 10 m/s |
| Recoating Speed | 400 mm/s — approx. 8 s per layer |
| Laser Type | Quad Lasers, 4×1000W with Beam Shaping, Quad Lasers, 4×500W, Six Lasers, 6×500W |
| Scanner | F theta lenses |
| Inert Gas Protection | Argon/Nitrogen |
| Average Inert Gas Consumption in Process | 3-5 L / min |
| Chamber Purge Time | 11 minutes (full chamber) |
| Operating system | 64 bit Windows 10 |
| Software | BuildStar, MakeStar® |
| Data File Format | STL |
| Key Software Features | Open machine key parameters, real-time build parameter modification, three-dimensional visualization, diagnostic functions |
| Power Supply | EUR/China: 400V±10%, 3~/N/PE, 50Hz, 42A · US: transformer supplied with the machine |
| Operating Ambient Temperature | 71.6-82.4 °F / 22-28 °C |
| Material | 17-4PH, 316L, AlSi10Mg, ST1, Ti-6Al-4V, 18Ni300 |
| Technology | Metal LPBF |
| Printing Materials | Metal Powders |
Product videos
Send your STL and we print a paid benchmark part on an FS350M-class system in California, with the parameter set and the cost per part written up.
Other products teams run alongside Farsoon FS350M LPBF Metal 3D Printer – 4×500 W, 4×1000 W or 6×500 W Lasers | 17.1×14.1×15.7 in / 433×358×400 mm
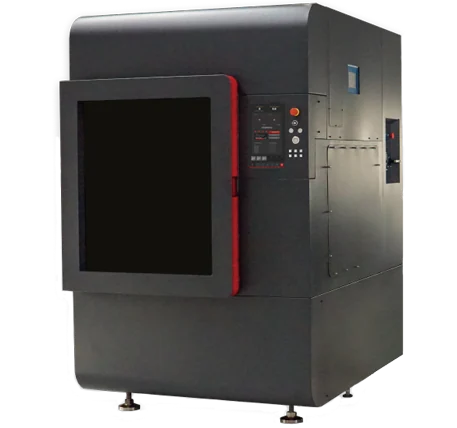
The InssTek MX-Fab is an all-in-one 5-axis DED metal 3D printer with a 31×39×28 in / 800×1000×700 mm work envelope — a 1,000 W (up to 2,000 W) ytterbium fiber laser, DMT closed-loop melt-pool control, and up to six powder feeders for multi-material and functionally graded parts.
- ✔ 5-axis DED with real-time DMT melt-pool feedback — dense, near-net-shape metal
- ✔ 30+ qualified alloys: Ti, Ni superalloys, stainless & tool steel, CoCr, Cu — multi-material in one build
- ✔ Fabrication, cladding, and repair on one platform
- ✔ Lead time: configured to order — request a quote for delivery & installation
Made to order
· Quote on request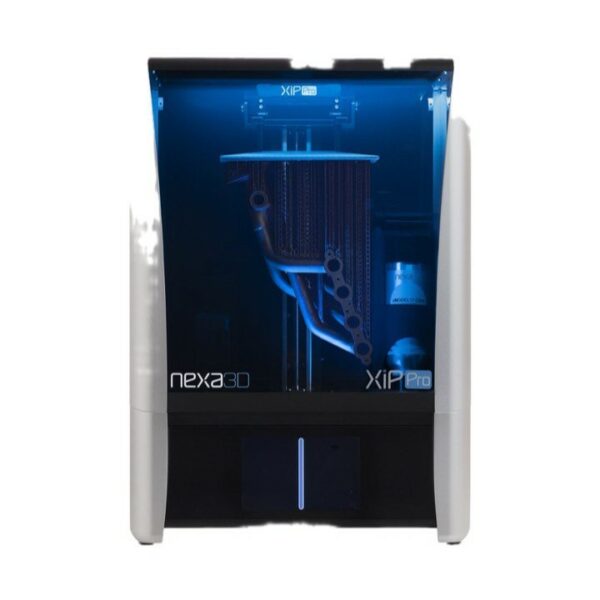
The XiP Pro is Nexa3D's industrial resin 3D printer — class-leading build volume and print speed for functional prototypes and end-use production at low cost per part.
- ✓ LCD-based LSPc (Lubricant Sublayer Photocuring) vat photopolymerization for accuracy and dimensional stability
- ✓ Class-leading build volume and print speed for high production throughput
- ✓ Runs validated and Open resins via NexaX Pro · full xWASH / xCURE post-processing available
Made to order
· Built to order — contact us for current lead time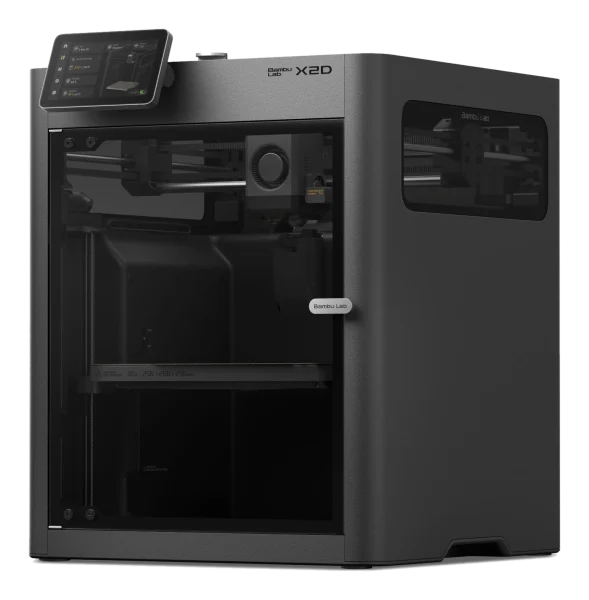
Dual-nozzle printing made accessible — two materials or colors in one print, clean low-waste supports, and a 65°C active-heated chamber in a compact 256 mm machine.
- Dual-nozzle — 2 materials/colors per print, cleaner supports, less waste
- 300°C hotend + 65°C active chamber — ABS, ASA, PC, PA
- Compact 256×256×260 mm enclosed build
- US additive experts · ships in 1–2 business days from US stock · pay over time with PayPal
- Price match against any authorized US dealer · POs, tax-exempt and EDU/GOV orders welcome
In stock
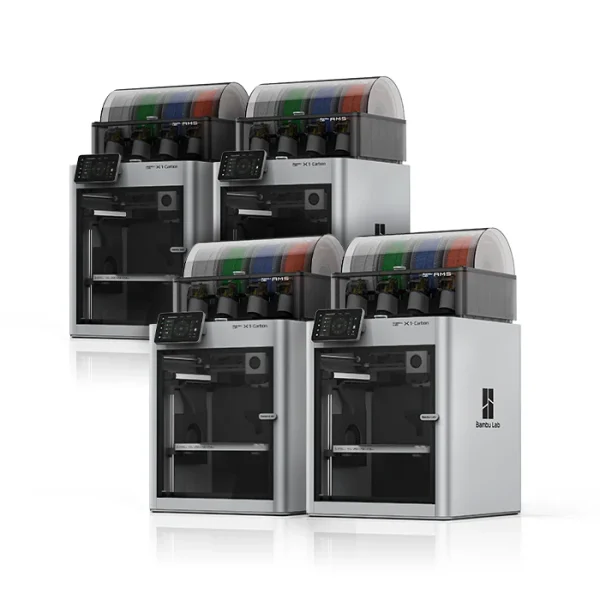
Expert on-site installation and hands-on operator training for your Bambu Lab printer, delivered by Additive Plus. Choose the session length that fits your team.
In stock
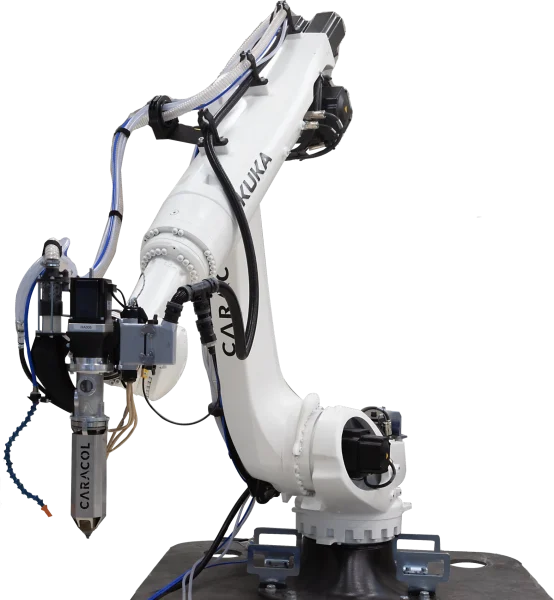
Heron AM configured with the High Accuracy (HA) extruder head — Caracol's 6-axis robotic large-format additive platform. 2 kg/h through 1–5 mm nozzles at up to 350°C, pellet-fed with optional hybrid CNC milling. EN9100 and ISO 9001 certified. Priced by configuration.
- ✓ 6-axis robotic LFAM — freeform geometries up to 15 m, beyond any gantry
- ✓ High Accuracy head: 2 kg/h, 1–5 mm, 350°C — fine detail, best surface finish
- ✓ EN9100 + ISO 9001 certified · lead time confirmed at quote
Made to order
· Lead time confirmed per configuration at quote. Talk to a specialist for a schedule.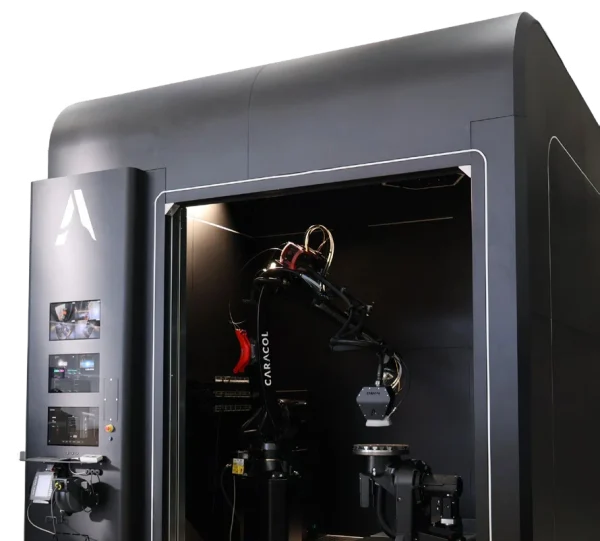
Vipra AM is Caracol’s turnkey robotic WAAM platform for metal production parts — a 9-axis cell running CMT (Cold Metal Transfer) deposition at up to 13.2 lb/h / 6.0 kg/h inside an 8.2 × 6.6 × 6.6 ft / 2.5 × 2.0 × 2.0 m envelope, across 11 qualified alloys from ER70S-6 steel to Inconel 625. CE marked. Priced by configuration.
- ✓ 9-axis architecture — robot, external manipulator and linear track, 1,650 lb / 750 kg positioner payload
- ✓ Closed-loop monitoring — pyrometer, layer geometry and gas flow correct parameters in-build
- ✓ Lead time: approx. 16 weeks — configured to order
Made to order
· Approx. 16 weeks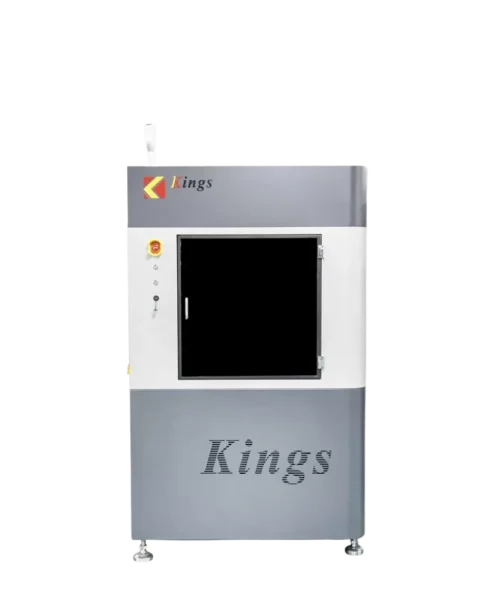
Mid-format industrial SLA. Marble frame. Vacuum recoating. Built for high-volume printing of footwear lasts, dental arch batches, engineering prototypes and patterns — without stitching or Z-seam artifacts.
- ✓ 26×26×16 in / 650×650×400 mm build chamber — nests a full tray of lasts or arches per run
- ✓ Solid-state 355 nm Nd:YVO4 laser · 0.075–0.8 mm variable beam · 15.0 m/s max scan
- ✓ Full-marble machine frame — thermal stability for ±0.1 mm part accuracy
- ✓ Lead time: 2–3 months — on-site install, calibration & operator training included
Made to order
· 2–3 months from order placement. Need it sooner? Talk to a specialist.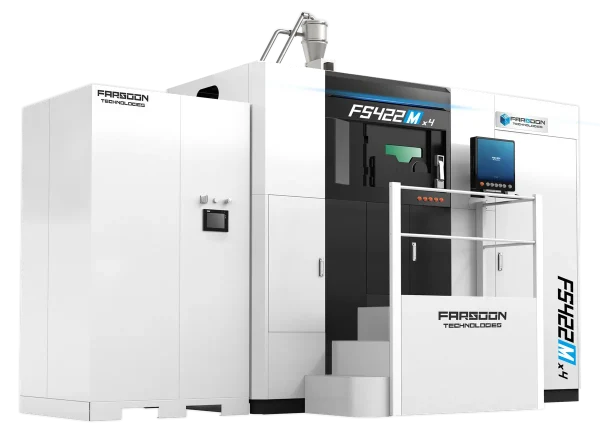
The Farsoon FS422M CAMS is a metal LPBF 3D printer with a 16.7×16.7×16.5 in / 425×425×420 mm build envelope, running a single 500 W laser or quad 500 W lasers.
- ✓ 150 cm³/h — volume build rate
- ✓ 16.7×16.7×16.5 in / 425×425×420 mm build envelope
- ✓ Open platform — full access to process parameters, qualify your own alloy
- ✓ Lead time: built to order — confirmed at quote
Installation and commissioning in the USA: facility and gas planning, start-up and operator training by our US service team.
Made to order
· Built to orderCommon questions
Don't see yours? Email [email protected] — NDA standard, typical reply within 4 hours.
Which alloys are qualified for the Farsoon FS350M?
Which laser configuration should we buy?
Is the FS350M open, or locked to vendor parameters?
What does installation in the USA involve?
How is powder handled between builds, and is it safe for Ti6Al4V?
What build rate can we expect in practice?
Can we test the machine before committing?
Place your order, or talk to an engineer first
Order Farsoon FS350M LPBF Metal 3D Printer – 4×500 W, 4×1000 W or 6×500 W Lasers | 17.1×14.1×15.7 in / 433×358×400 mm direct, or talk to materials engineer